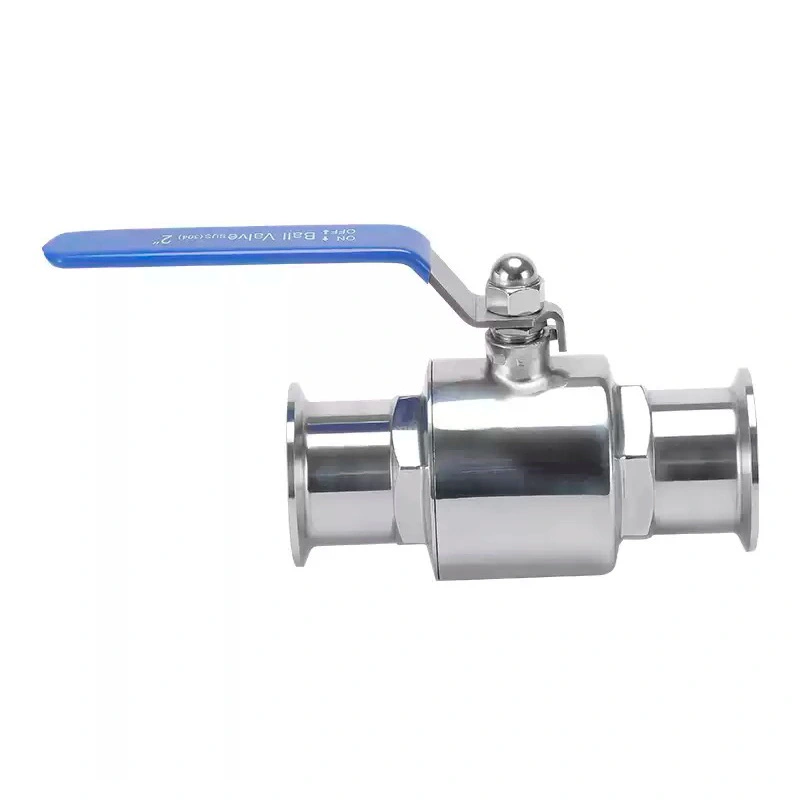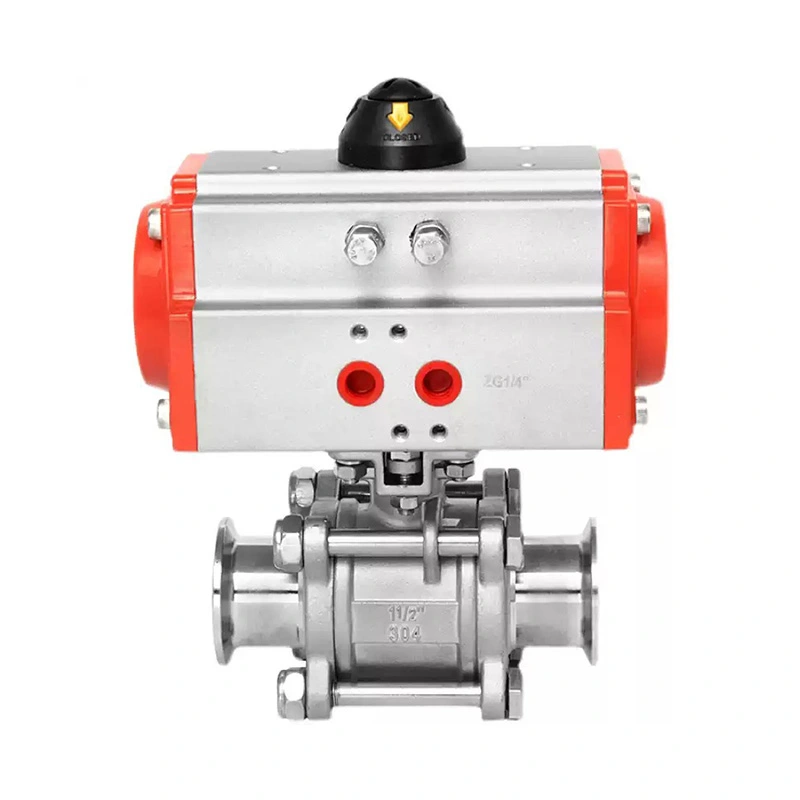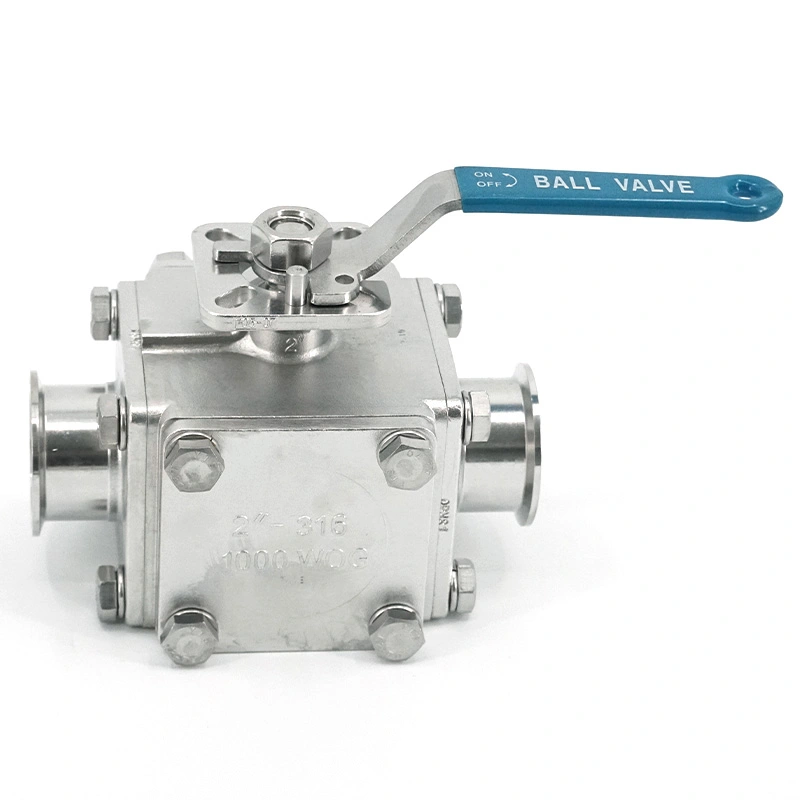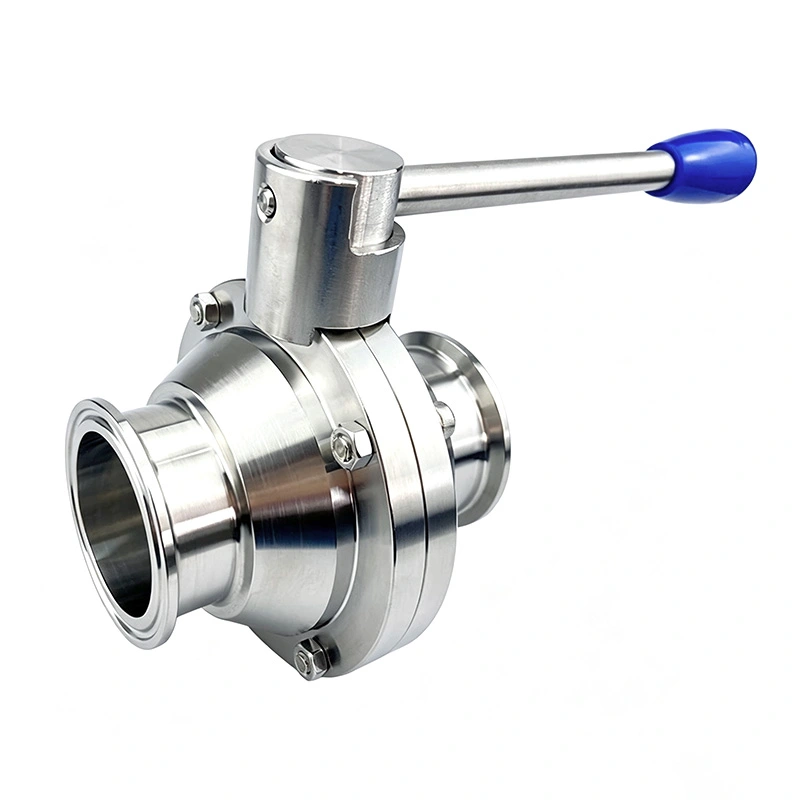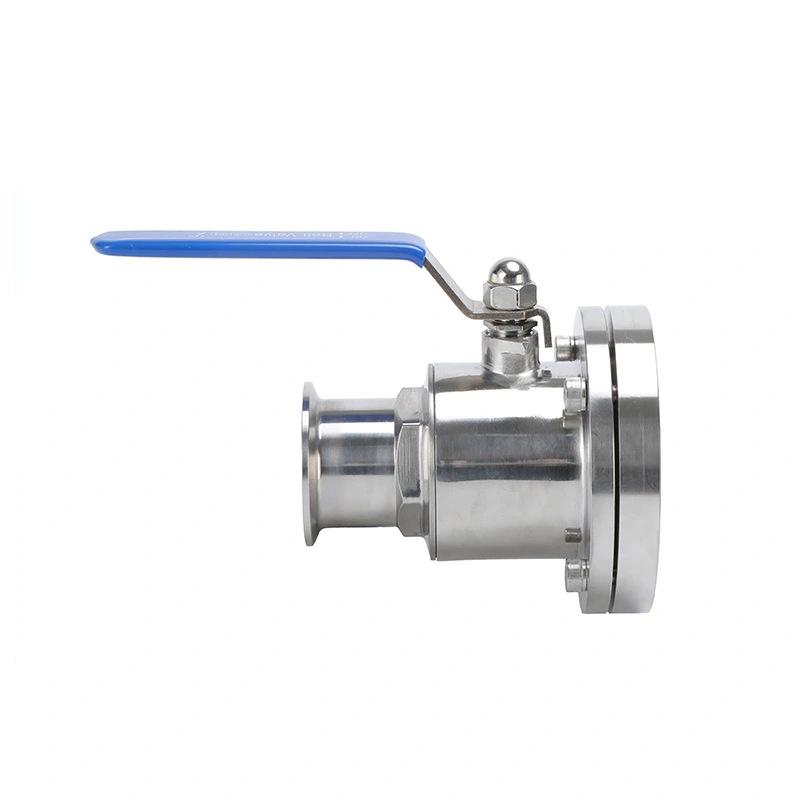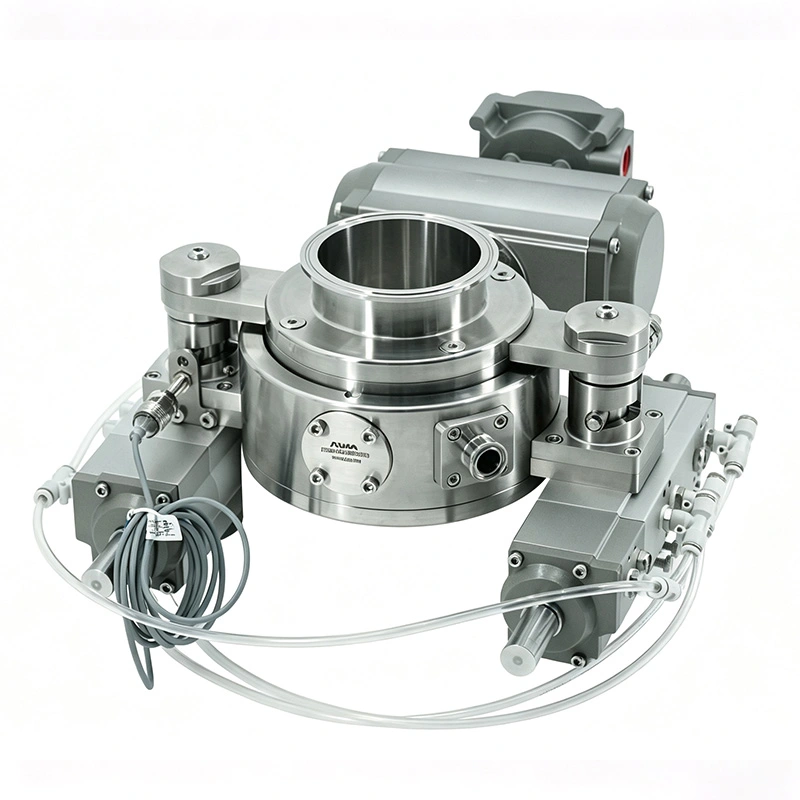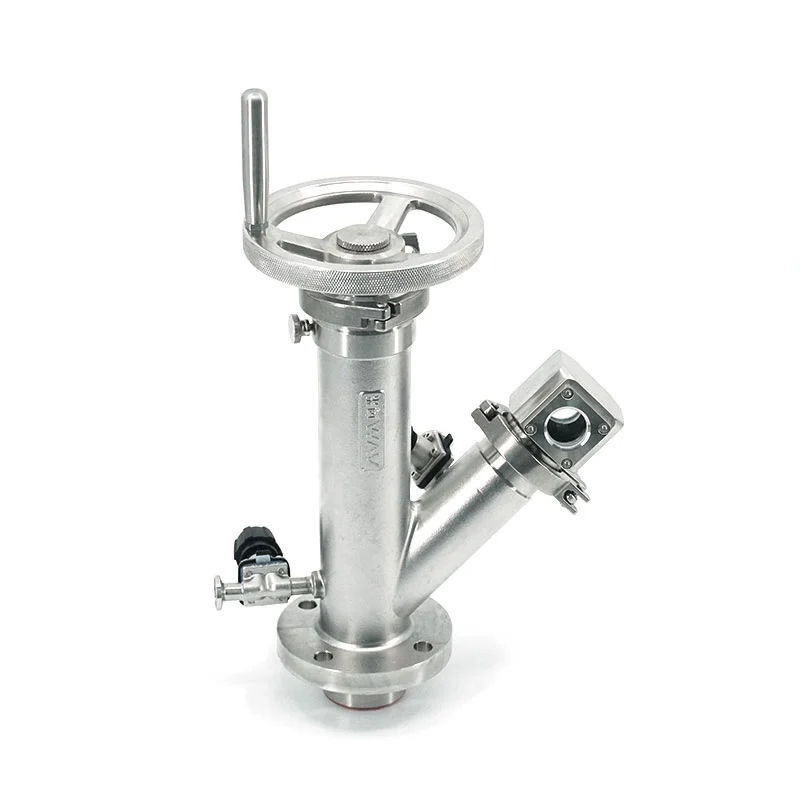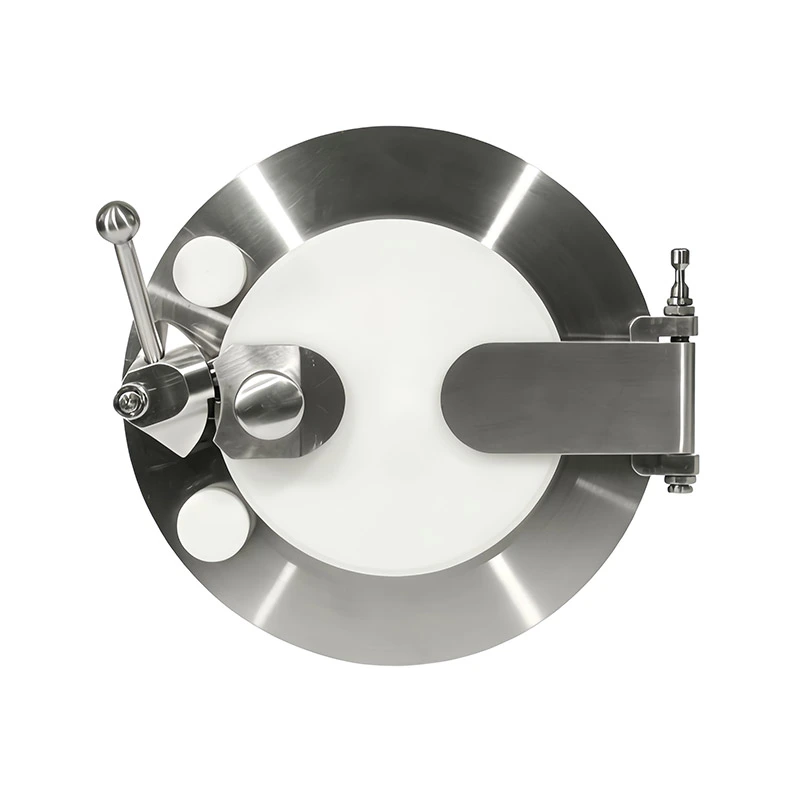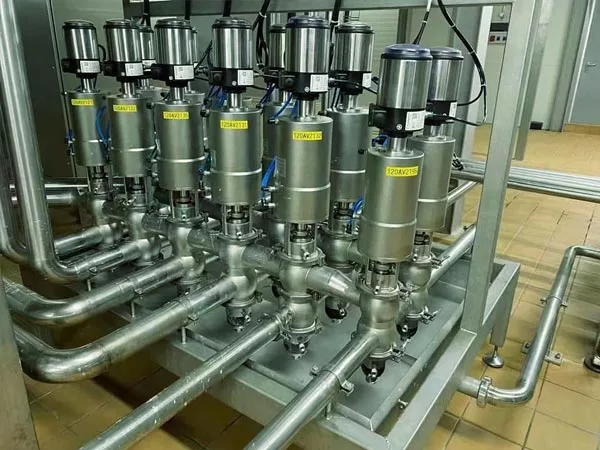
AVM provides sanitary flow control solutions for liquid processing systems that require efficient transfer, stable operation, and reliable pipeline control. Designed with a rotary ball structure, the valve provides a direct flow passage for process fluids while supporting quick operation and flexible installation. It is widely used in pharmaceutical, biotechnology, food & beverage, and other high-purity industries.
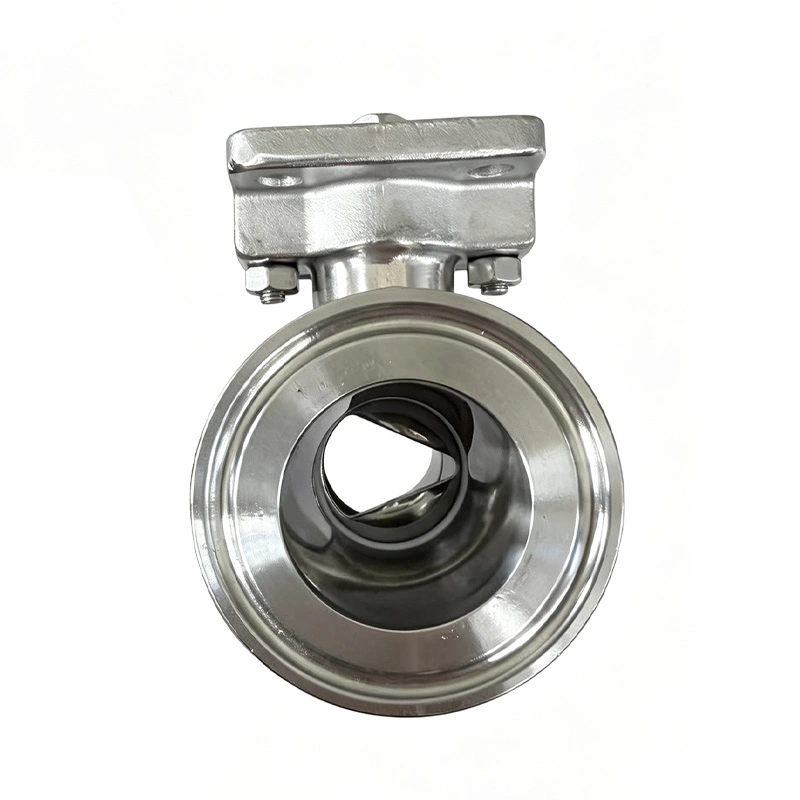
The internal passage design directly influences fluid movement and system efficiency. AVM's Sanitary Ball Valve adopts a full bore flow structure that helps reduce flow resistance and pressure loss during operation. This design is suitable for process systems requiring smooth liquid transfer and stable flow performance.
Compared with some traditional valve structures, ball valves provide a relatively open flow channel when fully opened. AVM designs its valves to support efficient fluid movement, making them suitable for applications where maintaining sufficient flow capacity is important. This helps improve the performance of liquid transfer systems and reduces unnecessary restrictions in pipelines.
Many processing systems require reliable isolation between different sections of a pipeline. The ball rotation mechanism allows the valve to provide clear opening and closing positions, supporting effective separation of process lines. The Sanitary Ball Valve can be used for liquid transfer, equipment connection, maintenance isolation, and process switching applications.
Different production environments require different operating methods. AVM ball valve solutions can be configured for manual operation or automated control according to system requirements. Pneumatic actuation options allow the valve to be integrated into automated processing lines where remote operation and synchronized control are needed.
Space utilization is an important consideration when designing modern processing equipment. The compact structure of AVM sanitary ball valves allows flexible installation in different piping layouts. This makes them suitable for process skids, filling systems, transfer lines, reactors, and other sanitary liquid handling equipment where installation space needs to be optimized.
The Sanitary Ball Valve can be applied in pharmaceutical liquid processing, biotechnology systems, food and beverage production, chemical processing, and other high-purity applications. Typical uses include liquid transfer, pipeline isolation, equipment connection, and process line control where reliable operation and efficient fluid handling are required.
Valve selection depends on factors including pipeline size, fluid characteristics, operating pressure, temperature range, connection requirements, and automation needs. AVM provides customized configurations to match different process conditions, helping customers choose suitable valve solutions for their production systems.
AVM Extraordinary Intelligent Control Co., Ltd. provides sanitary valve solutions for pharmaceutical, biotechnology, food, and other demanding industries. With ISO 9001, CE, and FDA certifications, AVM supports global customers with reliable valve products designed for high-purity processing environments.