Founded as AVM Fluid Equipment Technology Co., Ltd., specializing in sanitary valves, sanitary fittings, and fluid control systems for high-purity applications in the pharmaceutical, food & beverage, and biopharmaceutical industries.
2003
Certified with the ISO 9001 Quality Management System and 3-A Sanitary Standards certification, reinforcing commitment to international quality and hygiene standards.
2005
Established the international business division and expanded exports to Germany, Japan, Italy, Brazil, South Korea, and Middle East markets.
2006
Became the first company in China to obtain a patent for the Split Butterfly Valve (SBV), strengthening innovation leadership in sterile containment technology.
2011
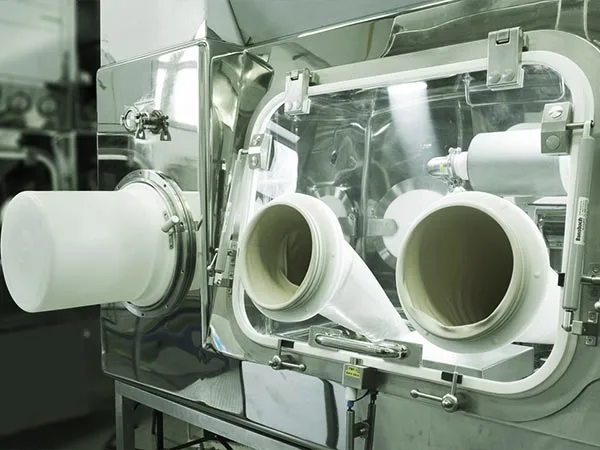
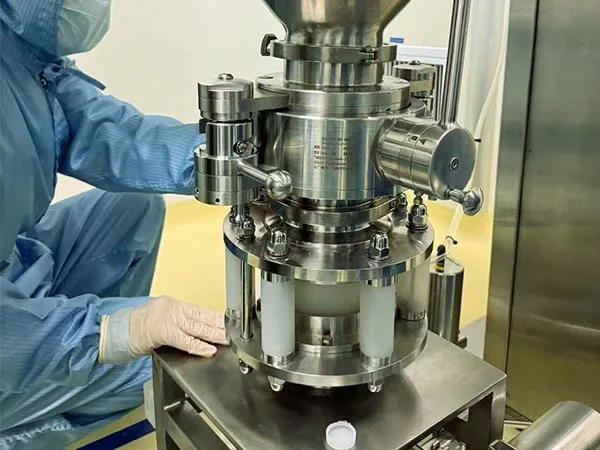
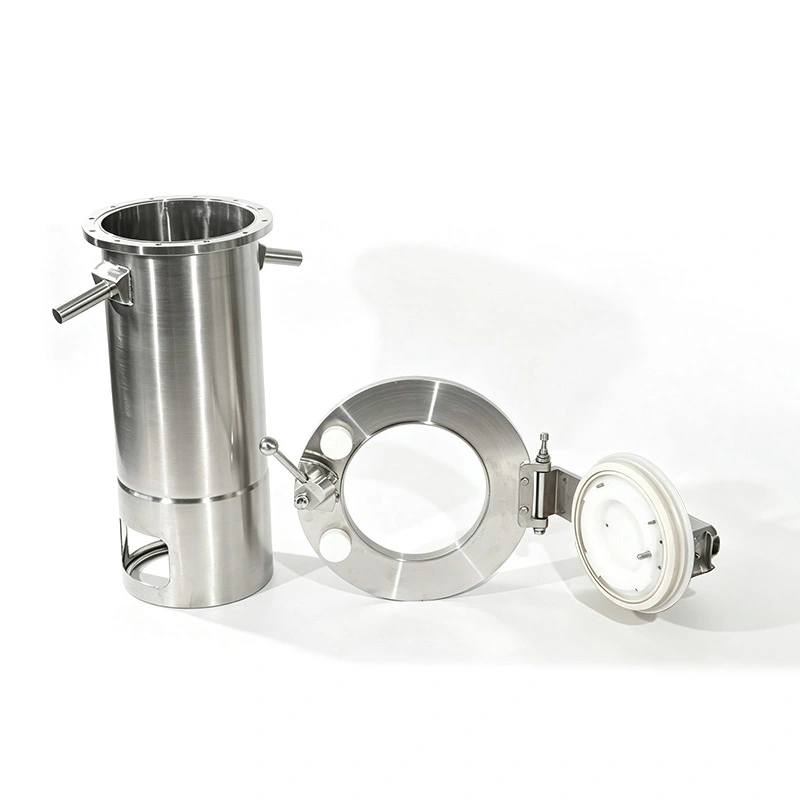
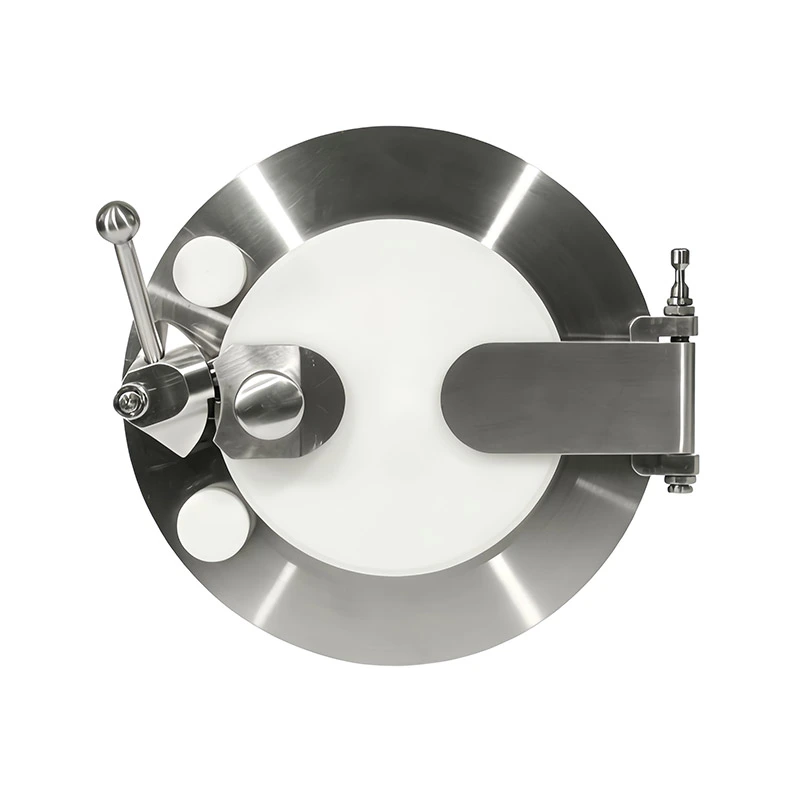
Focused on aseptic containment powder transfer solutions, including Split Butterfly Valves (SBV) and Rapid Transfer Ports (RTP), providing safe handling solutions for sterile, toxic, and hazardous materials.
2015
Introduced advanced Japanese Mazak CNC machines,US Wheeler and Korean high-precision machining centers to improve manufacturing accuracy, product consistency, and production efficiency.
2016
Launched a global brand strategy dedicated to sterile containment transfer solutions for pharmaceutical and high-cleanliness industries worldwide.
2020
Officially renamed to AVM Extraordinary Intelligent Control Equipment Co., Ltd., marking a new stage in intelligent fluid control and sterile containment system development.
2023
Expanded into new energy industry applications, successfully exporting Split Butterfly Valve (SBV) systems to lithium battery manufacturing projects in Finland.
2025
Participated in major international exhibitions in Algeria, Mexico, Egypt, Italy, and India, while strengthening global customer engagement through business visits across the Americas, South Korea, and Middle East regions.
2026
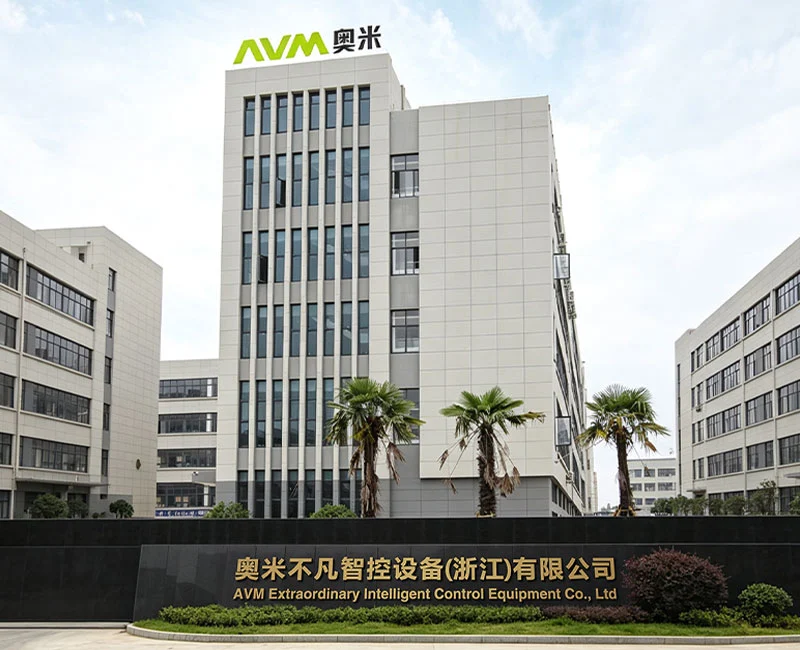
Founded in 2003, AVM Extraordinary Intelligent Control Equipment Co., Ltd. (formerly Aomi Fluid) has specialized in sanitary valve manufacturing and high-containment powder and liquid handling solutions for more than 20 years. The company began developing and manufacturing Split Butterfly Valves (SBV) in 2011 and became one of the earliest Chinese manufacturers and patent holders of split valve technology. With over 15 years of experience in powder transfer and containment systems, AVM has established strong technical expertise in aseptic processing, high-containment applications, and contamination control for critical industries. In 2025, AVM further expanded into the new energy sector, successfully delivering split valve solutions for lithium battery material handling projects in Europe.
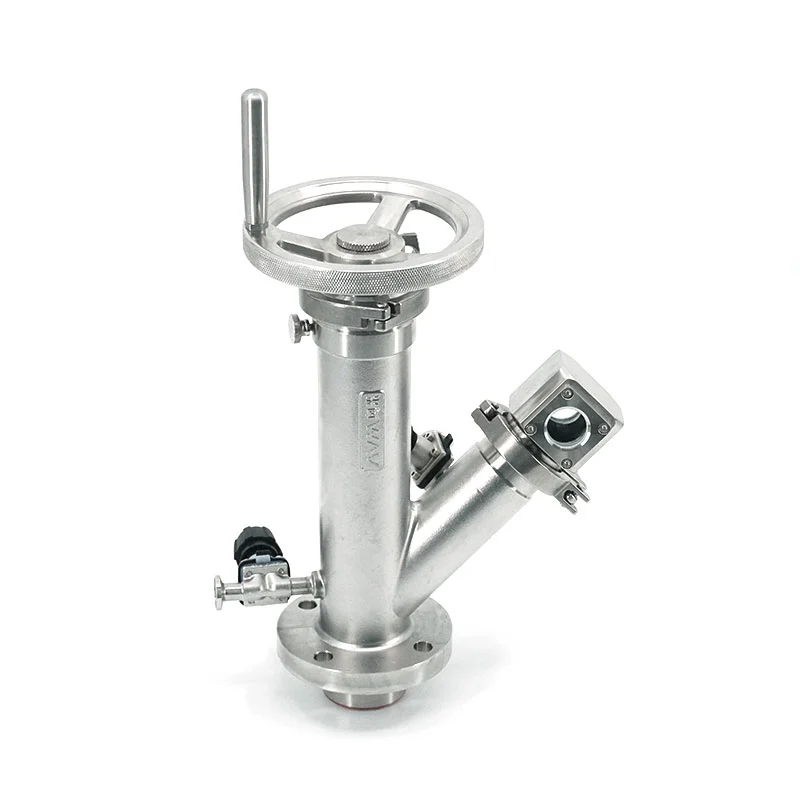
AVM Intelligent Control Equipment Co., Ltd. is a professional manufacturer focused on advanced containment systems and sterile powder handling equipment. The company serves global customers in the pharmaceutical, biotechnology, food processing, fine chemical, and lithium battery industries. AVM provides a complete range of intelligent containment products, including OEB5 Split Butterfly Valves (SBV), Rapid Transfer Ports (RTP), rotary valves, powder butterfly valves, dome valves, and customized containment solutions for demanding production environments.
Designed for handling highly potent, toxic, hazardous, and contamination-sensitive materials, AVM products help customers achieve safe, efficient, and GMP compliant production processes. The company places strong emphasis on operational safety, aseptic performance, and reliable containment technology to support modern pharmaceutical and industrial manufacturing requirements.
All AVM products are manufactured in accordance with international standards such as ISO, DIN, and 3-A sanitary standards, while production and quality management systems comply with GMP and FDA requirements. Supported by advanced engineering capabilities, precision manufacturing equipment, and strict quality control procedures, AVM is committed to delivering reliable, high-performance, and regulatory-compliant containment solutions for global process industries.
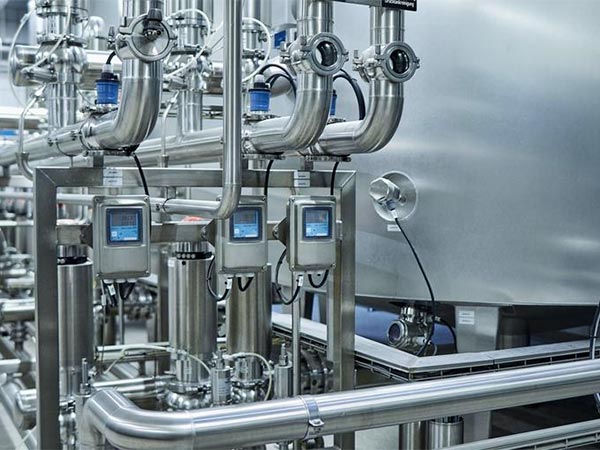
CIP (Clean-in-Place) and SIP (Sterilization-in-Place) systems are widely used in the pharmaceutical, food & beverage, and biotechnology industries for automated cleaning and sterilization of equipment and pipeline systems. Sanitary valves feature excellent temperature resistance, corrosion resistance, and hygienic dead-leg-free designs, helping improve system cleanliness, reduce manual maintenance costs, and enhance production efficiency and process reliability.
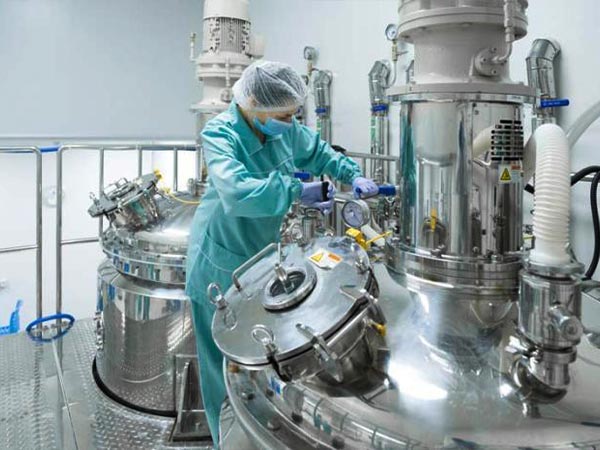
GMP cleanroom systems are extensively used in pharmaceutical, biotechnology, and high-end manufacturing industries to control air cleanliness, microbial contamination, and cross-contamination risks. The integration of sanitary valves and hygienic process equipment helps maintain sterile production environments, improve product quality and operational safety, and meet the stringent standards of modern clean manufacturing.
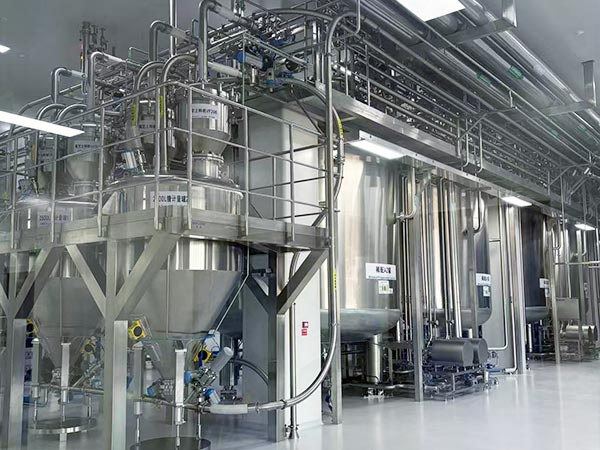
Sanitary stainless steel piping systems are widely applied in pharmaceutical, food processing, biotechnology, and fine chemical industries for the transportation and control of high-purity fluids and clean media. Manufactured from high-quality stainless steel materials, these systems offer excellent corrosion resistance, easy cleaning performance, and high-temperature resistance, improving overall process stability and hygienic standards.
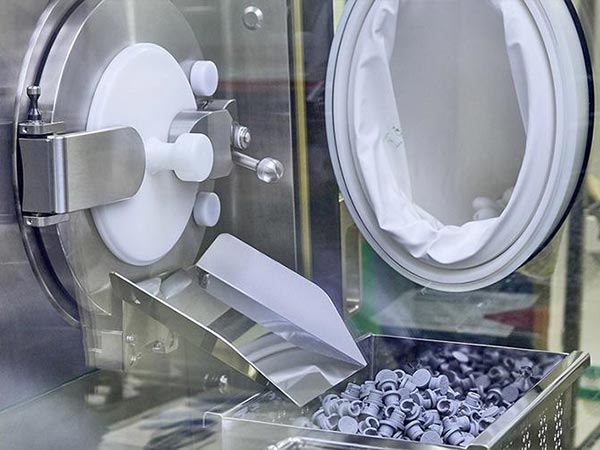
In Pharmaceutical & biopharmaceutical sterile drug manufacturing processes, sanitary valves are widely used in aseptic fluid transfer systems, solution preparation systems, fermentation systems, and clean process pipelines. With excellent sealing performance and full CIP/SIP compatibility, these products comply with strict GMP and FDA requirements, ensuring safety, cleanliness, and stability throughout pharmaceutical production processes.
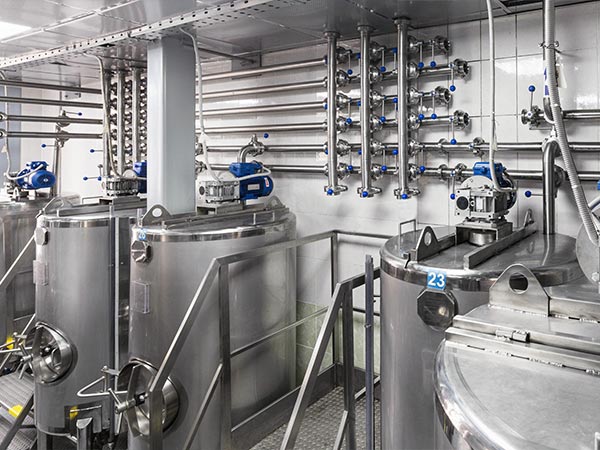
Sanitary valves are widely used in dairy, juice, beer, beverage, and liquid food production lines to ensure hygienic safety during conveying, mixing, filling, and cleaning processes. Made from food-grade stainless steel materials, these valves comply with international sanitary standards, effectively reducing contamination risks, improving production efficiency, and supporting clean manufacturing requirements in the modern food and beverage industry.
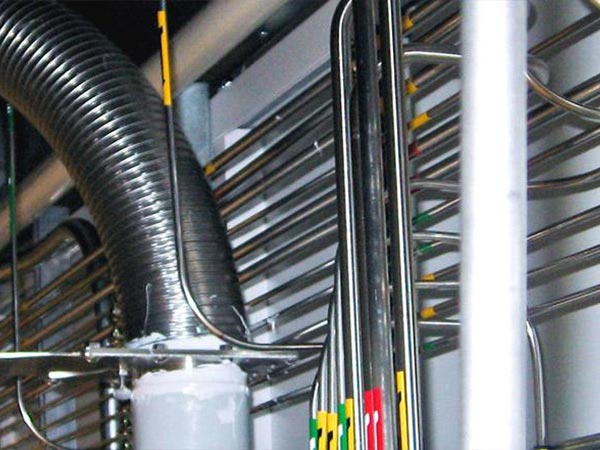
Sanitary valves are increasingly used in containment control and clean transfer systems for new energy materials, high-purity chemicals, and lithium battery manufacturing processes. Their high sealing performance, corrosion resistance, and easy-to-clean structure meet the strict requirements of the new energy industry for purity, stability, and automated production. These solutions are suitable for lithium battery materials, electrolytes, hydrogen energy systems, and fine chemical manufacturing applications.