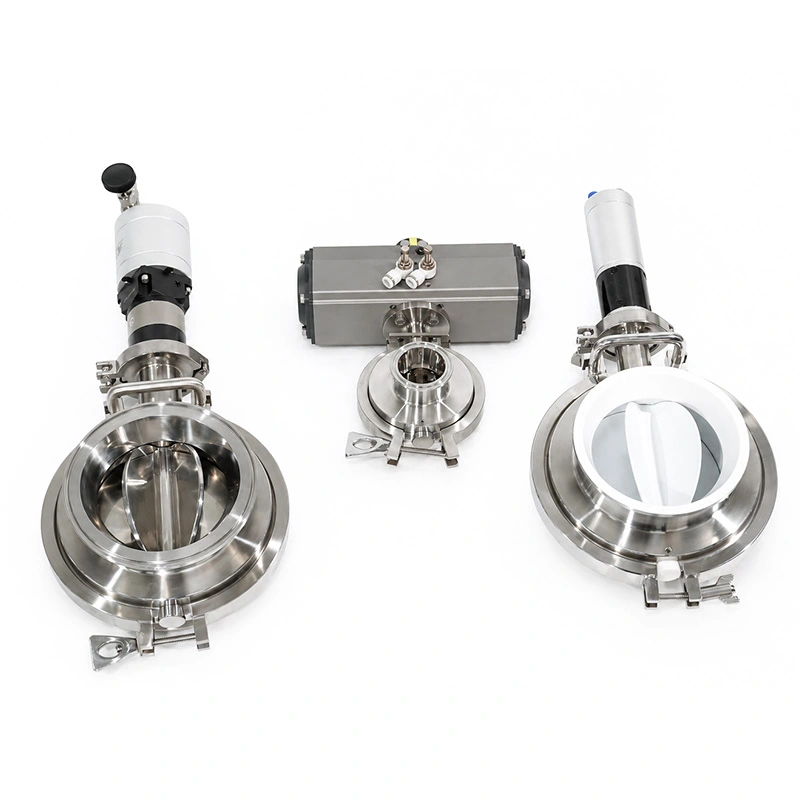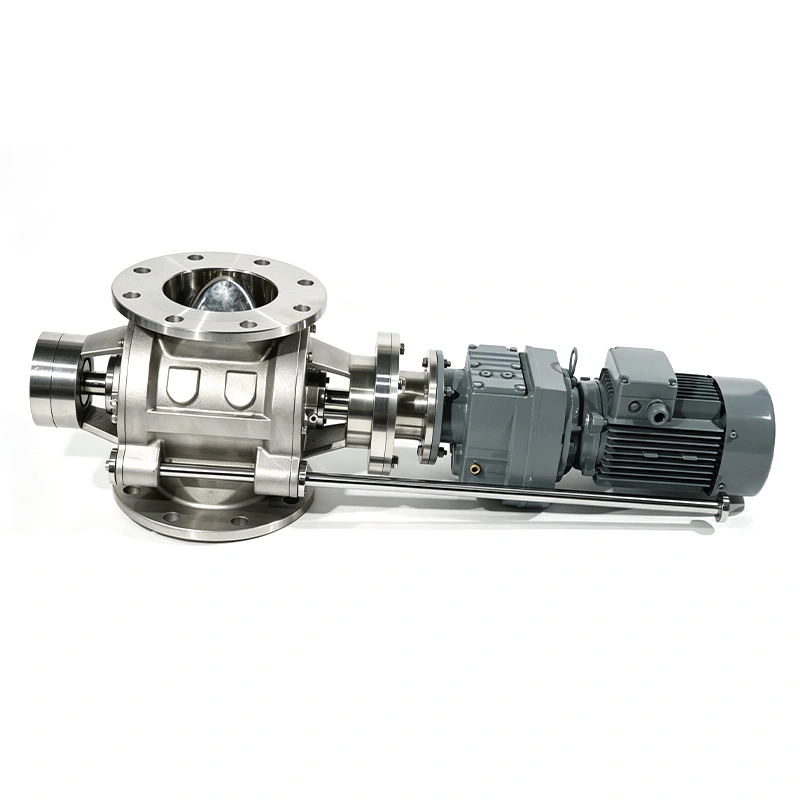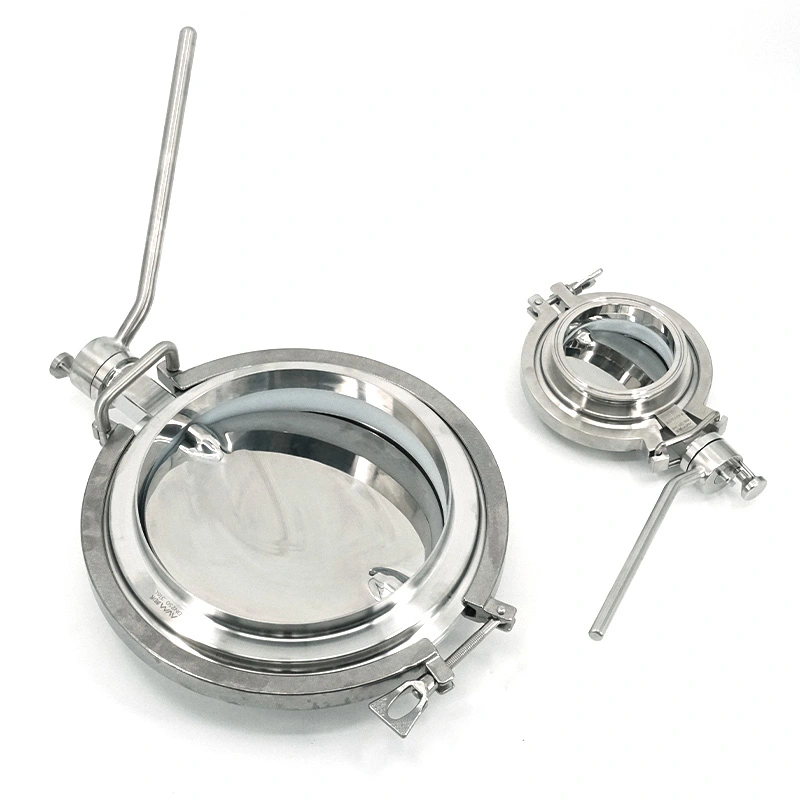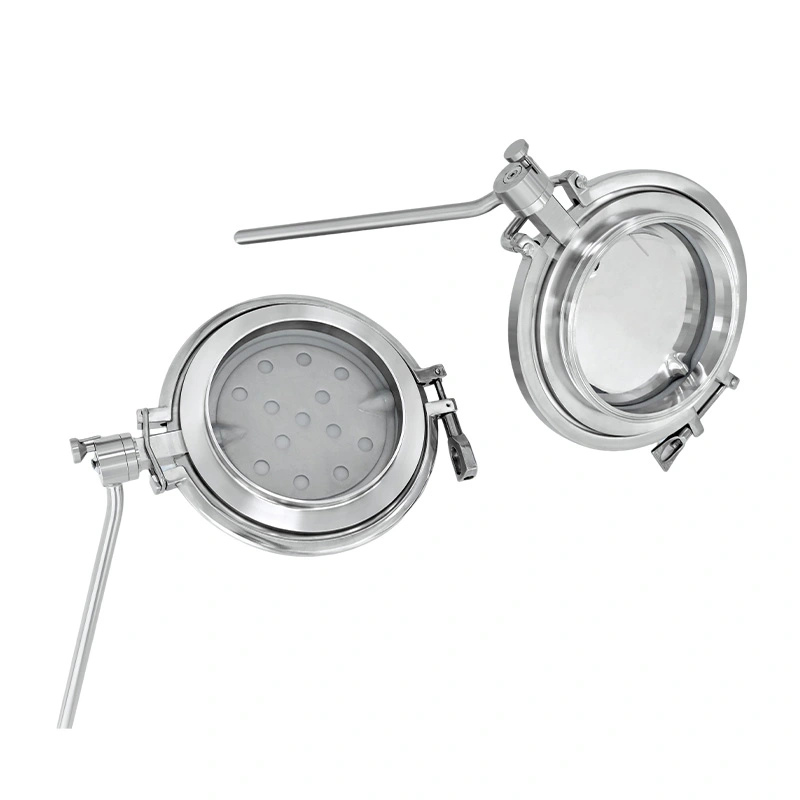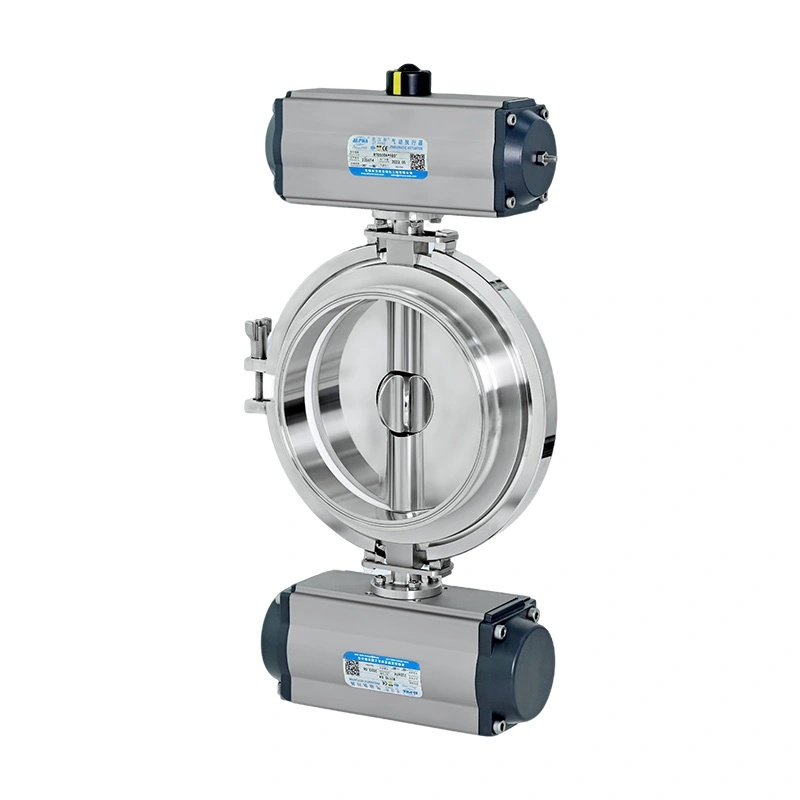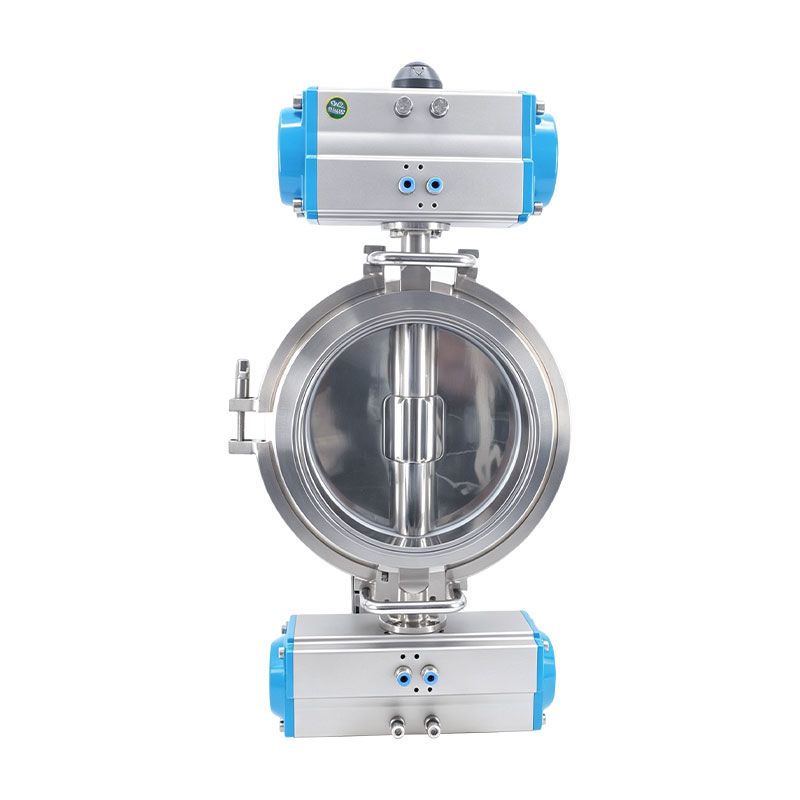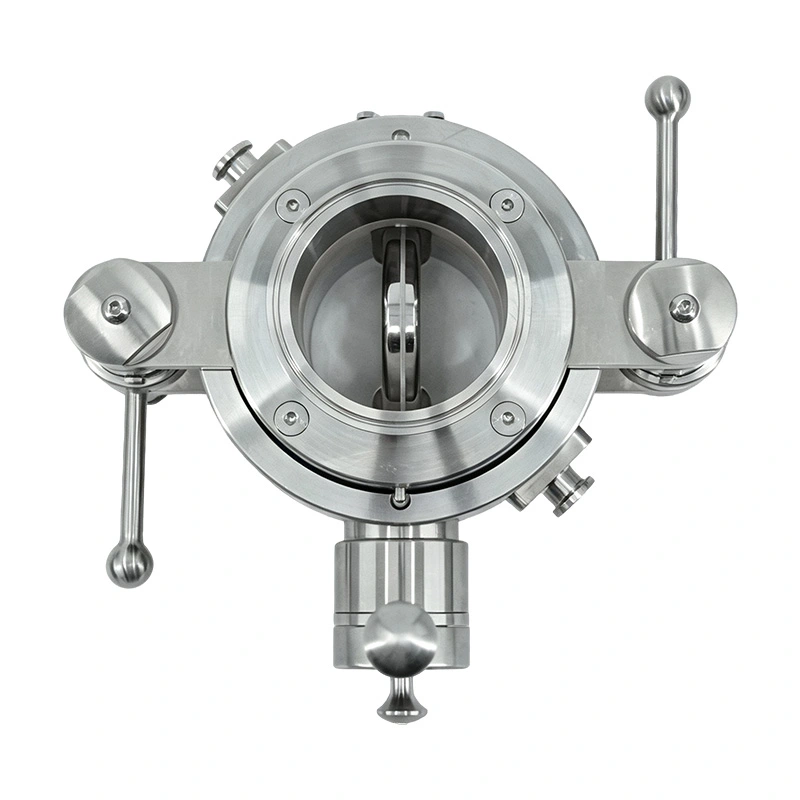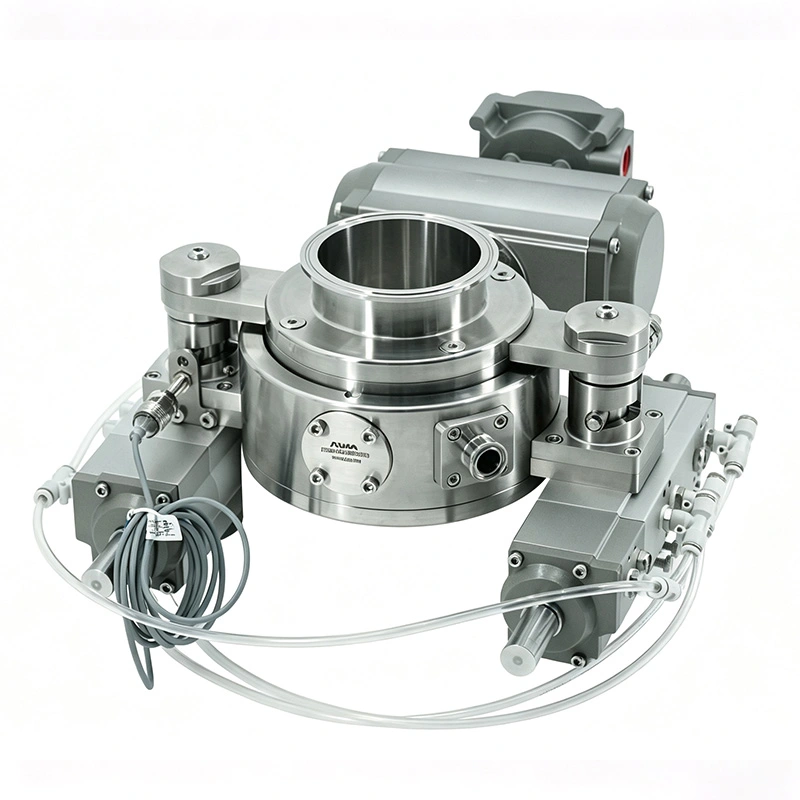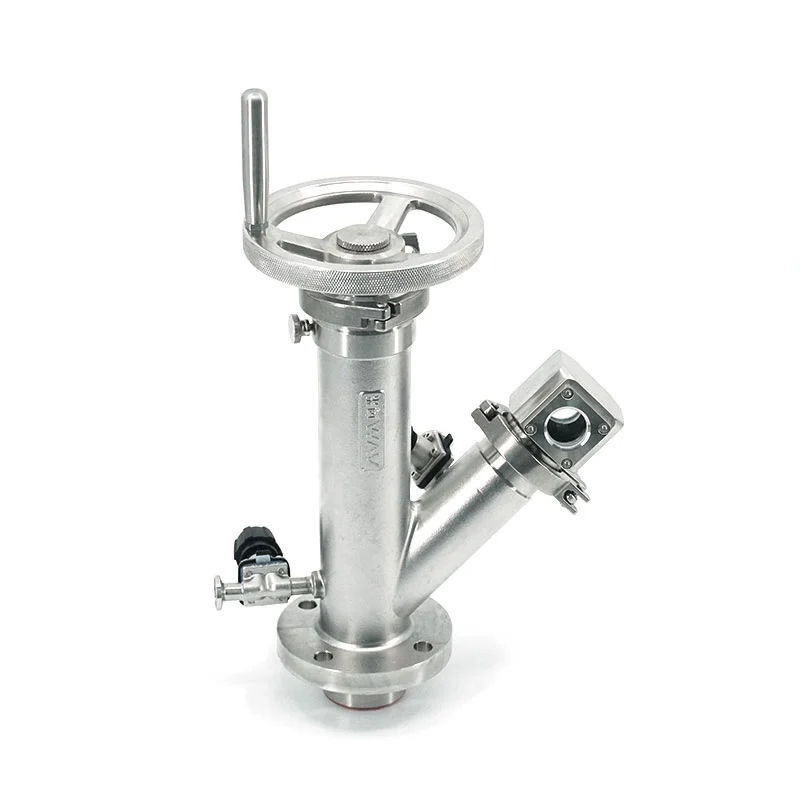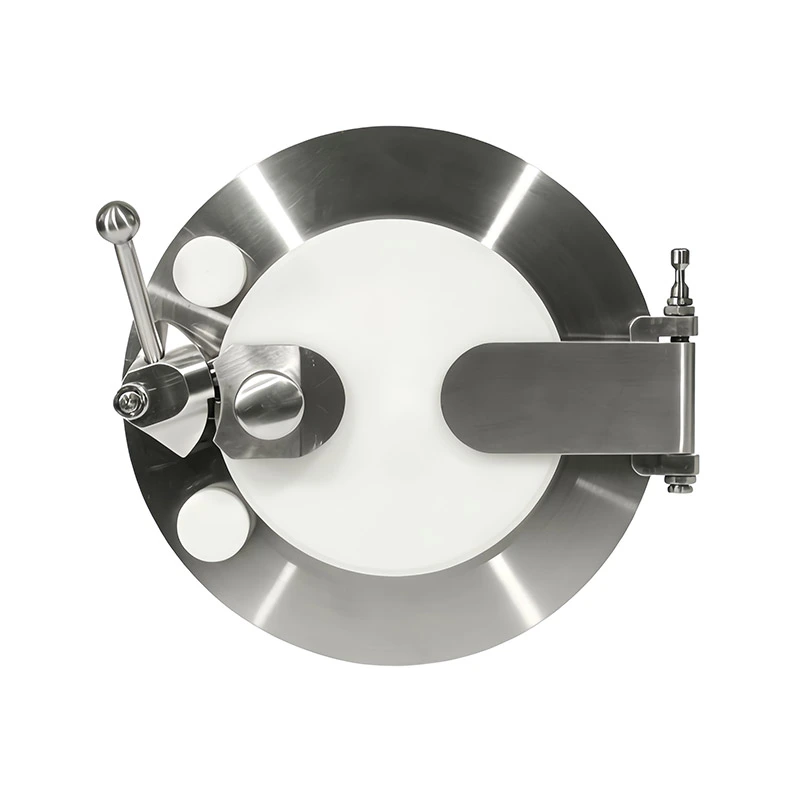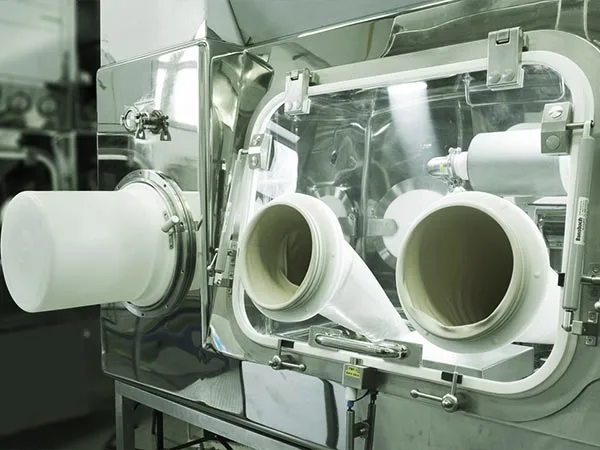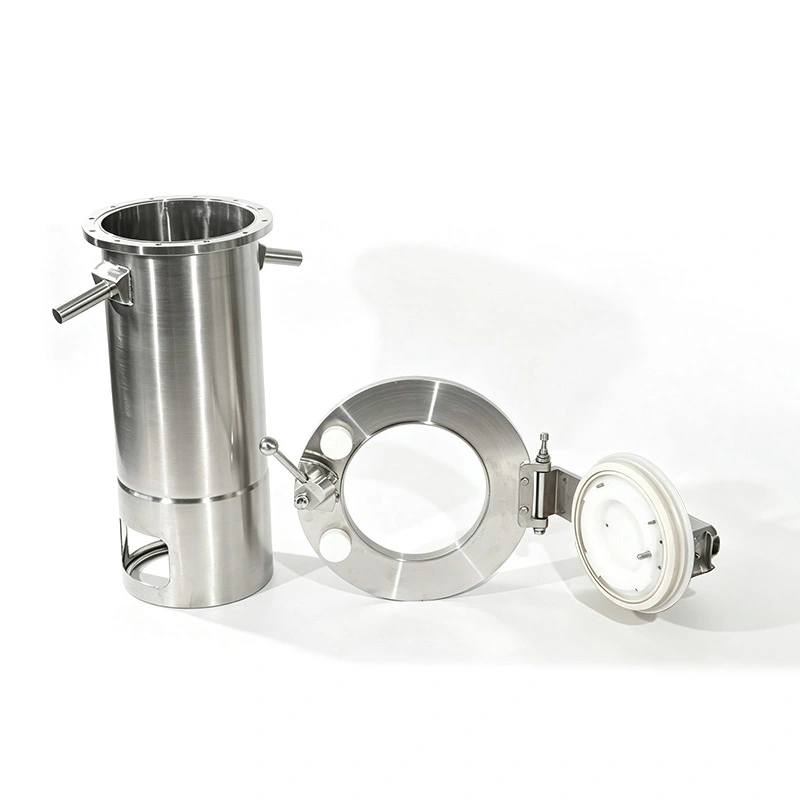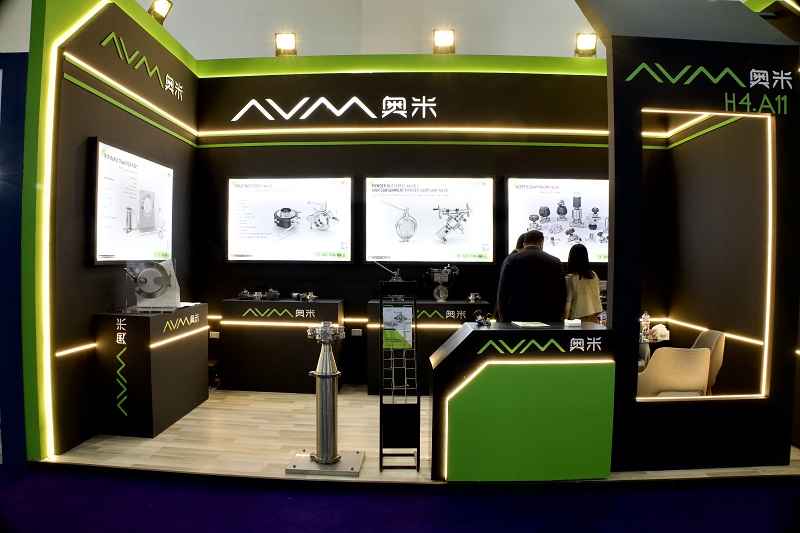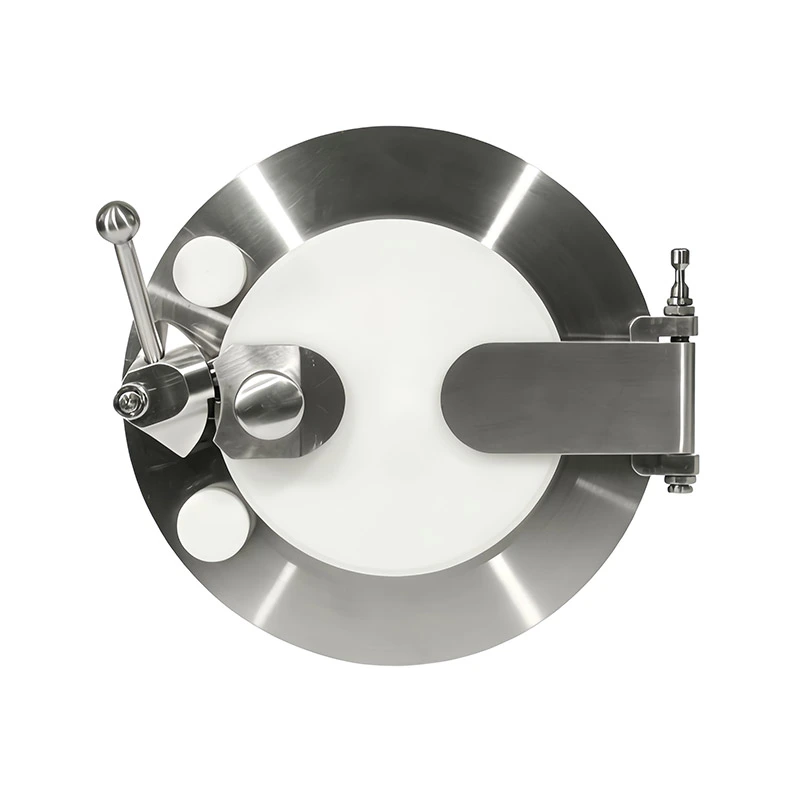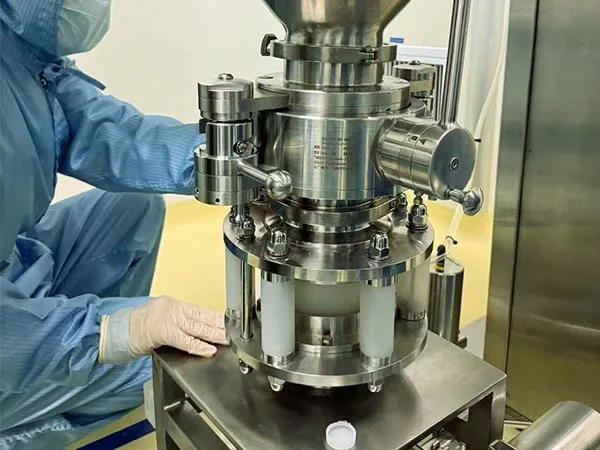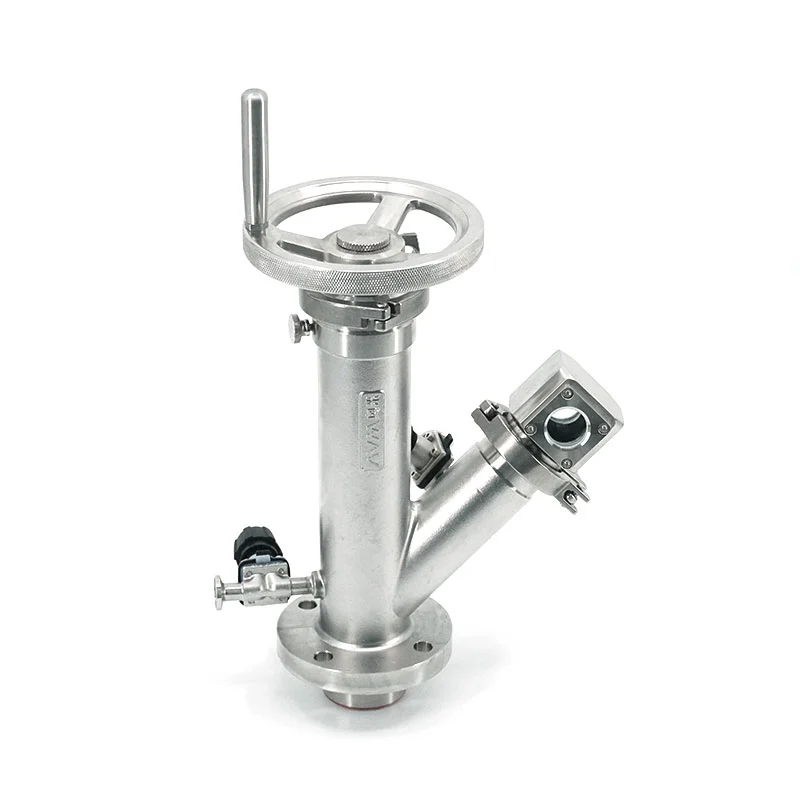
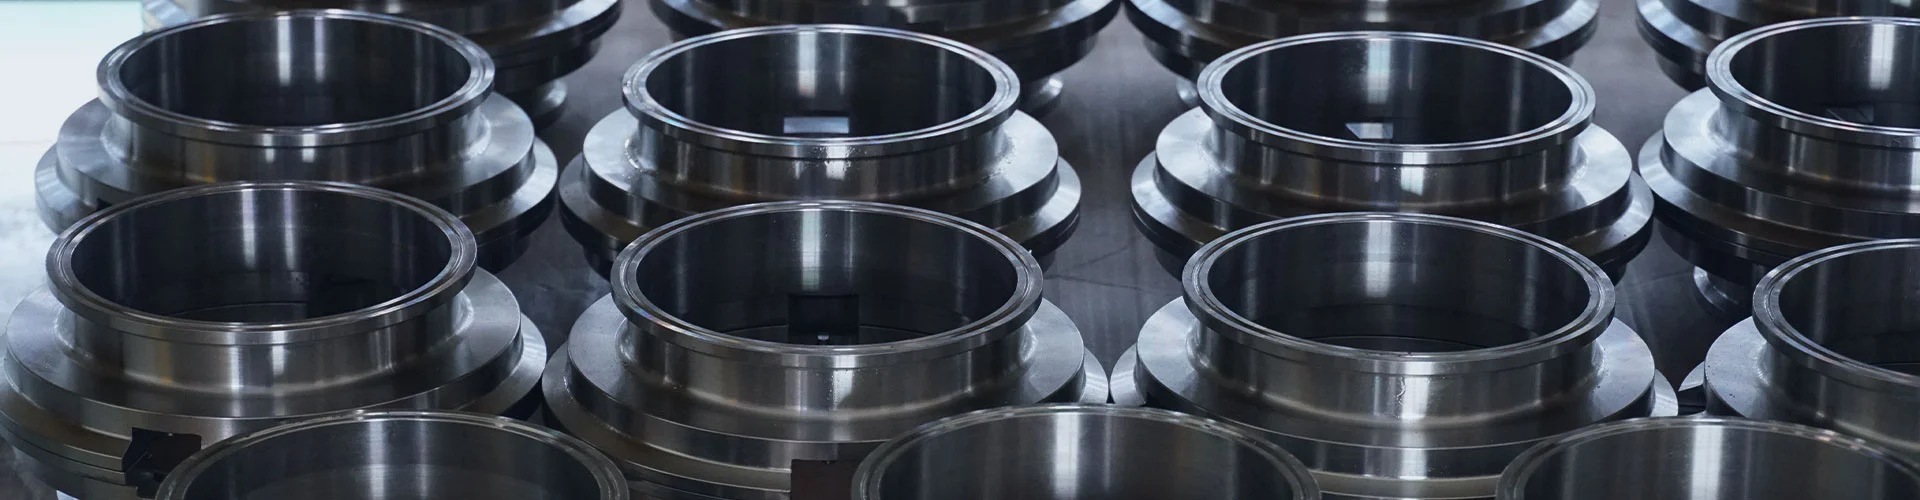
AVM supplies sanitary powder flow-control equipment for pharmaceutical, food and beverage, fine chemical, and lithium battery processing. Its range includes easy-clean powder butterfly valves, expansion butterfly valves, powder knife valves, and segment valves. These configurations are developed for powder conveying, discharge, isolation, and equipment connection, with attention to material flow, internal residue, cleaning efficiency, and long-term operating stability.
Powder behaves differently from liquid during conveying and discharge. Fine particles can accumulate around sealing areas, while cohesive or moisture-sensitive powders may create bridging and flow interruption. AVM designs its sanitary powder handling valve range around these process conditions, helping manufacturers choose a valve structure that matches powder properties, conveying methods, and pipeline arrangements.
Material retention is an important consideration when the same processing equipment handles different powder batches. Valve geometry and internal accessibility can affect how much material remains after operation. AVM's sanitary designs focus on reducing difficult-to-reach areas and making routine cleaning more practical, helping production teams shorten cleaning work and improve batch changeover efficiency.
Different powder operations call for different valve structures. Easy-clean powder butterfly valves are suitable for general powder isolation and transfer duties. Expansion butterfly valves can be selected when sealing and controlled opening characteristics are important. Powder knife valves provide a practical solution for shut-off applications, while segment valves can be integrated into powder processing systems requiring specific flow-control arrangements.
A sanitary powder handling valve should match more than the pipe connection. Buyers also need to consider powder particle size, bulk density, flowability, operating frequency, cleaning procedures, installation orientation, and available space. AVM can provide valve configurations according to these process conditions, making the equipment easier to integrate into existing or newly designed powder handling lines.
Pharmaceutical manufacturers can use these valves in powder transfer and discharge systems where clean processing is required. Food and beverage plants can apply them to powdered ingredients and dry-material conveying lines. Fine chemical production may require dependable isolation for different powder materials, while lithium battery manufacturing can use sanitary valve configurations in controlled powder processing and material transfer systems.
AVM Extraordinary Intelligence Control Co., Ltd. is located in Wenzhou, China, and integrates design, development, production, and sales. The company specializes in sanitary valves and powder handling equipment and has experience serving pharmaceutical, food and beverage, fine chemical, and lithium battery industries. AVM holds ISO 9001, CE, and FDA certifications, providing international buyers with references for product quality and compliance.