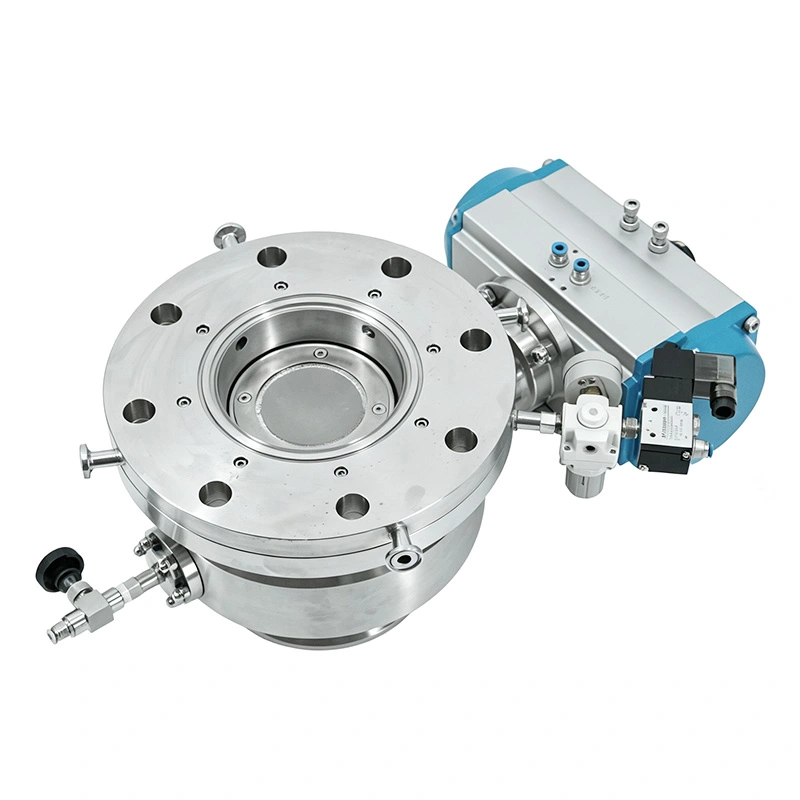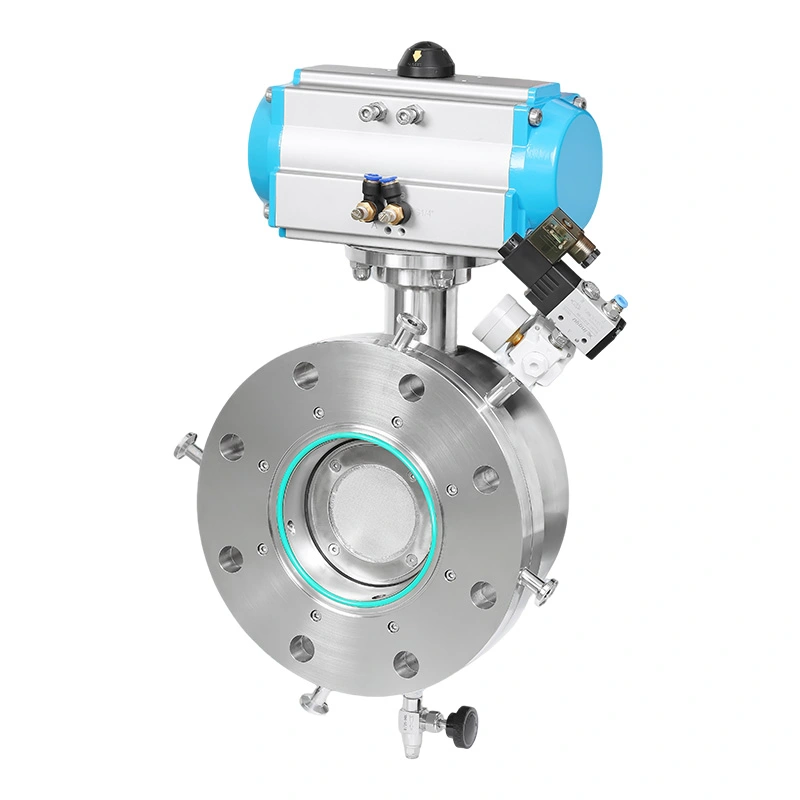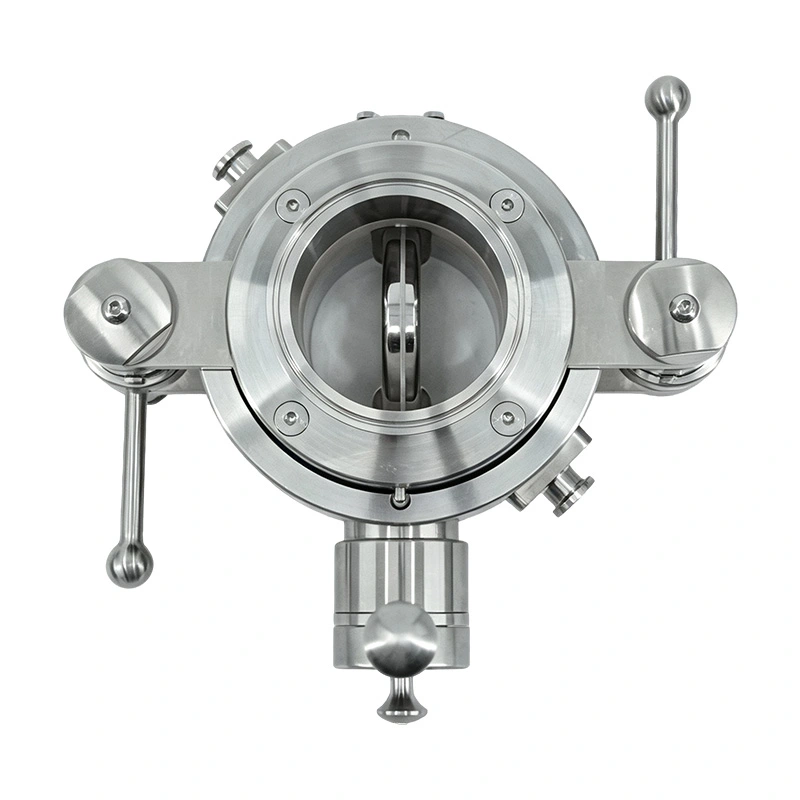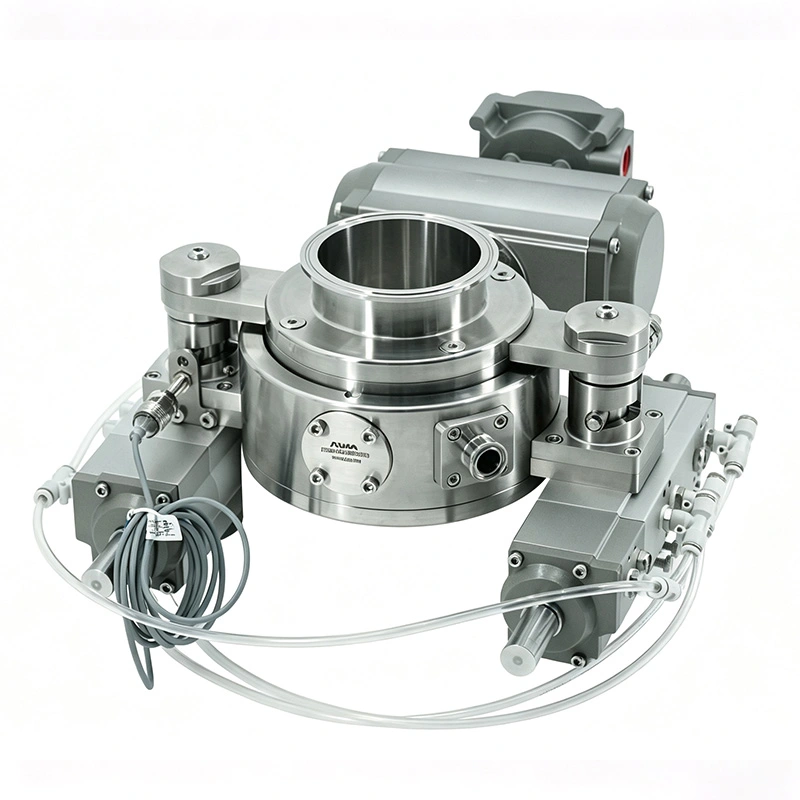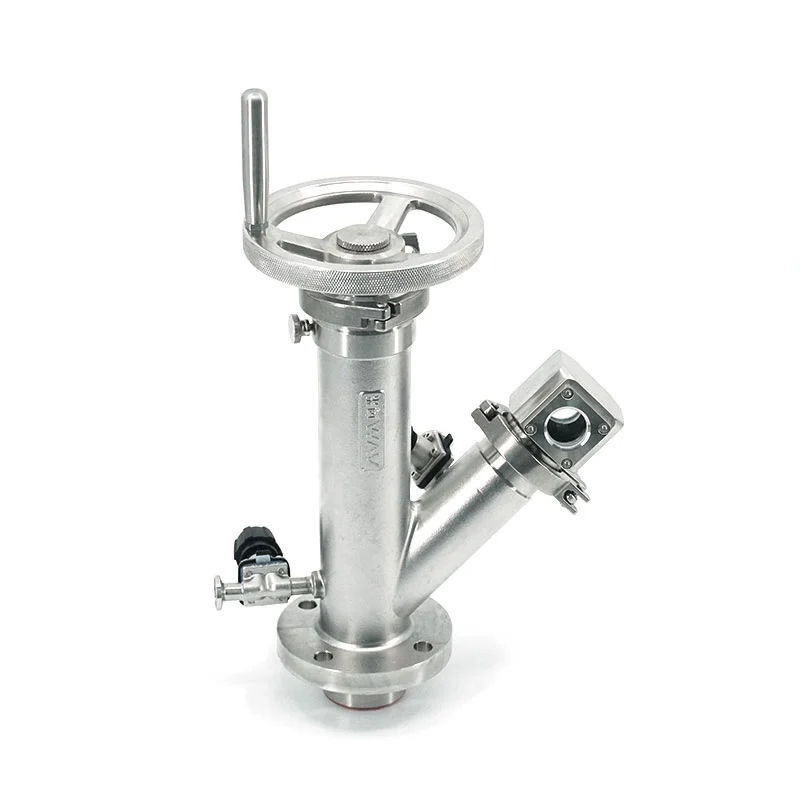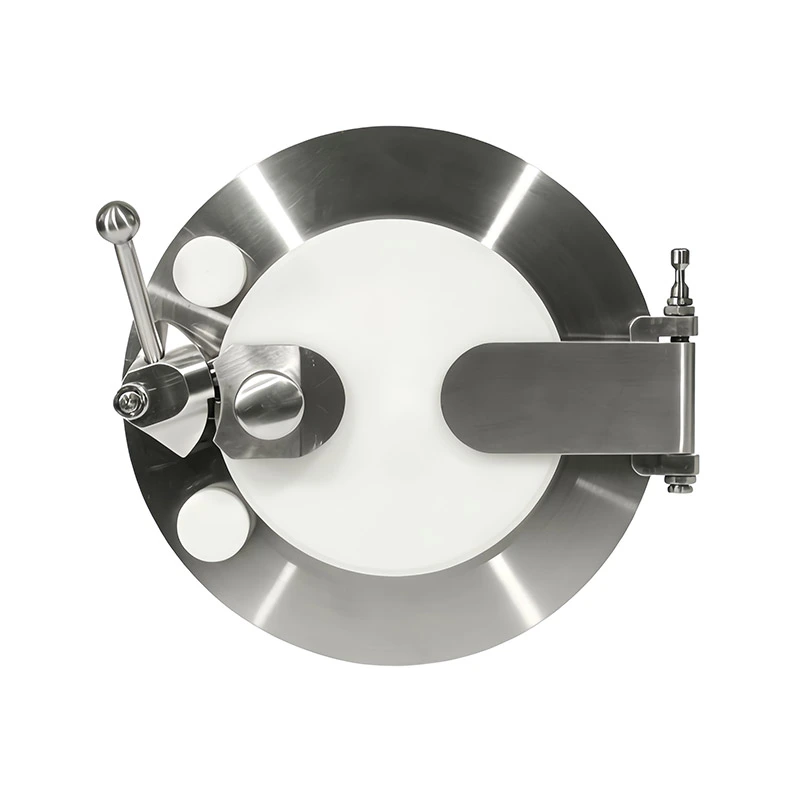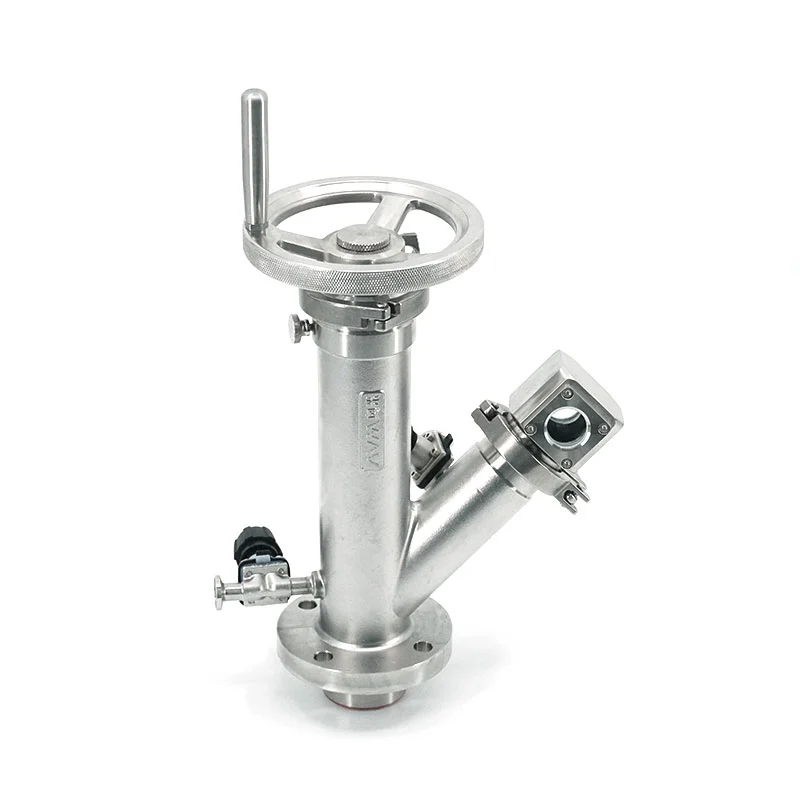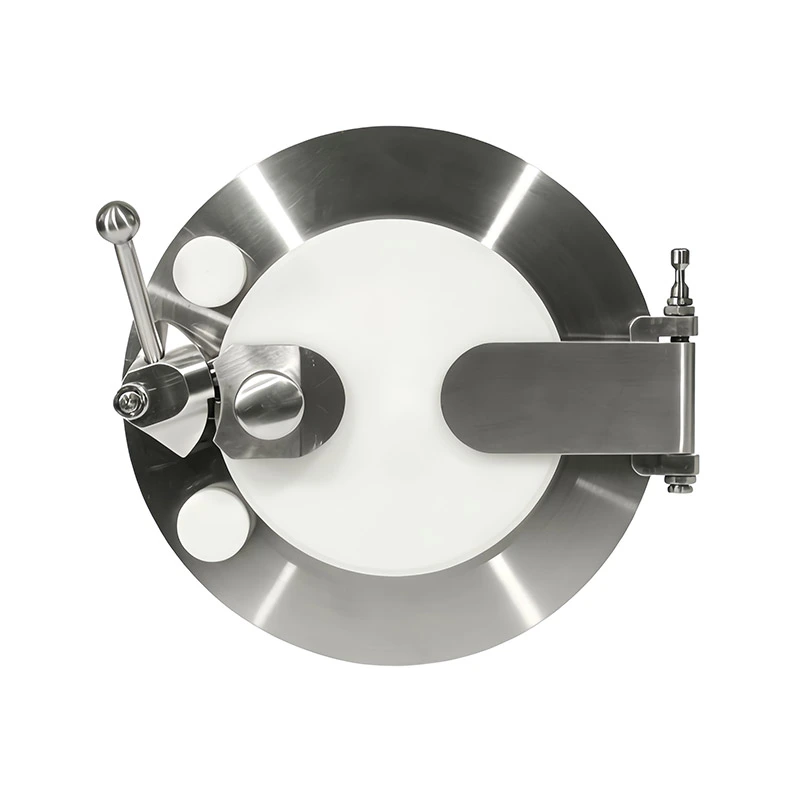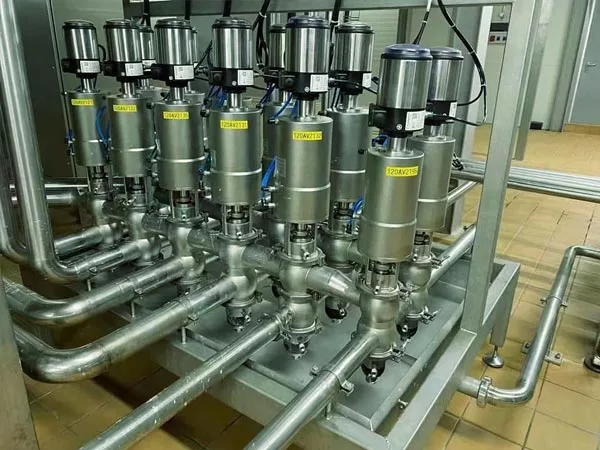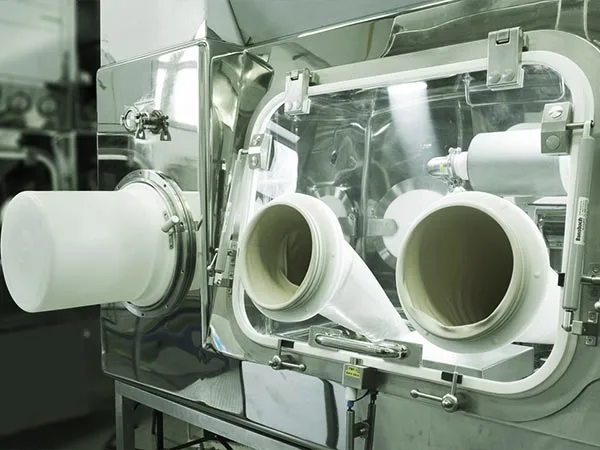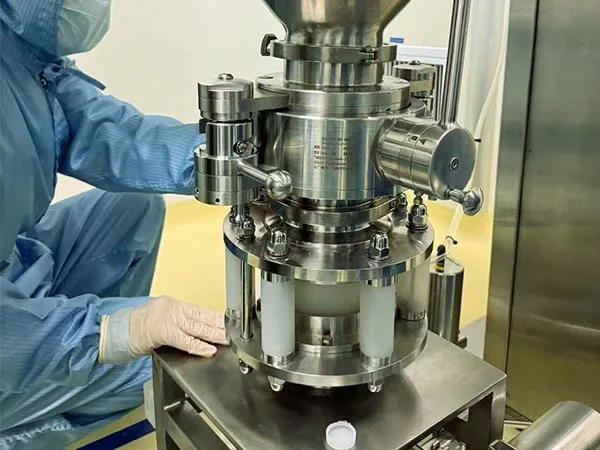
AVM provides sanitary valve solutions for applications requiring precise flow control and reliable media handling. The segment ball valve is designed with a specialized ball structure that allows efficient regulation of liquids, slurries, and process media containing particles. It is suitable for pharmaceutical, biotechnology, food & beverage, fine chemical, and other industries where hygienic design and stable process control are required.
Flow control requirements can vary significantly between different production processes. AVM's Sanitary Segment Ball Valve uses a segment-style flow passage to provide controlled regulation characteristics compared with traditional shut-off valve designs. This makes it suitable for applications where accurate adjustment of process media flow is required rather than simple opening and closing.
Some process fluids contain suspended particles, crystals, fibers, or high-viscosity components that may affect conventional valve operation. The segment ball structure provides a wider and more direct flow path, helping reduce potential blockage caused by material accumulation. The Sanitary Segment Ball Valve can therefore be applied in processes involving complex media conditions.
The internal flow passage of a valve influences pressure loss, energy consumption, and overall system performance. AVM optimizes valve geometry to support smoother media movement through the valve chamber. This design helps maintain efficient flow conditions and provides stable operation during continuous production processes.
For industries with strict cleanliness requirements, valve surfaces and internal structures are important factors in equipment selection. AVM uses sanitary construction principles with suitable product-contact materials and precision manufacturing processes. The design helps support easier cleaning procedures and reliable integration into hygienic processing systems.
The Sanitary Segment Ball Valve can be used in pharmaceutical liquid processing, biotechnology systems, food ingredient handling, fine chemical production, and other applications involving demanding process media. It is suitable for mixing systems, reaction processes, dosing lines, and pipeline control applications where stable flow adjustment is required.
Different production environments require different valve specifications. AVM can provide configurations according to operating pressure, temperature, media characteristics, connection requirements, cleaning methods, and installation conditions. This allows customers to select a valve solution that matches the actual process system instead of relying on a standard configuration.
AVM Extraordinary Intelligence Control Co., Ltd. is located in Wenzhou, China, and specializes in sanitary valve design, development, manufacturing, and technical support. The company provides valve solutions for pharmaceutical, biotechnology, food & beverage, and chemical industries. AVM holds ISO 9001, CE, and FDA certifications, supporting international buyers in evaluating sanitary process equipment suppliers.
For projects requiring a Sanitary Segment Ball Valve, AVM can provide suitable configurations based on flow control requirements, media characteristics, and process integration conditions.