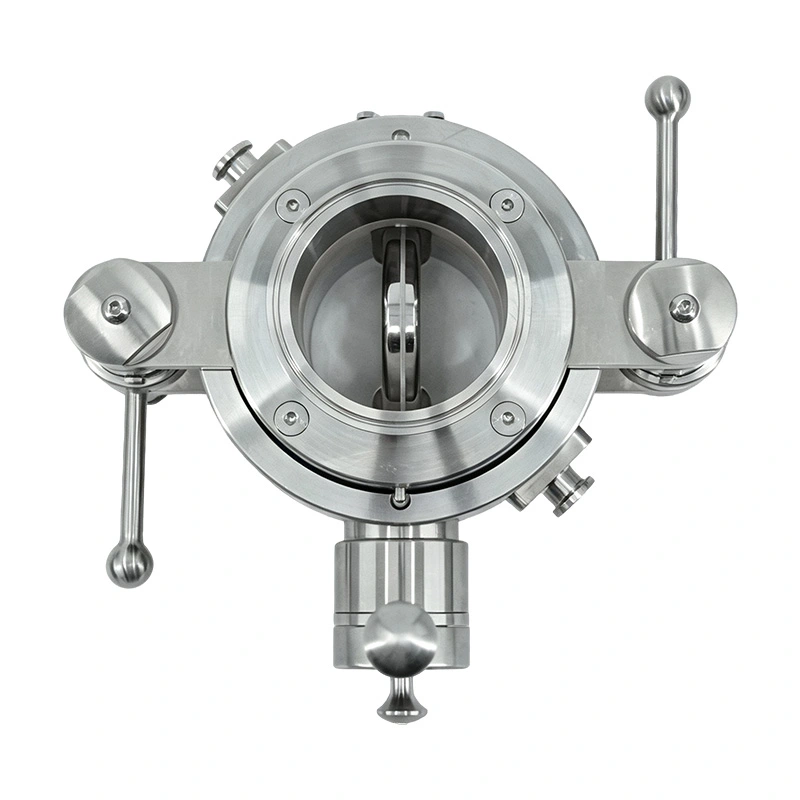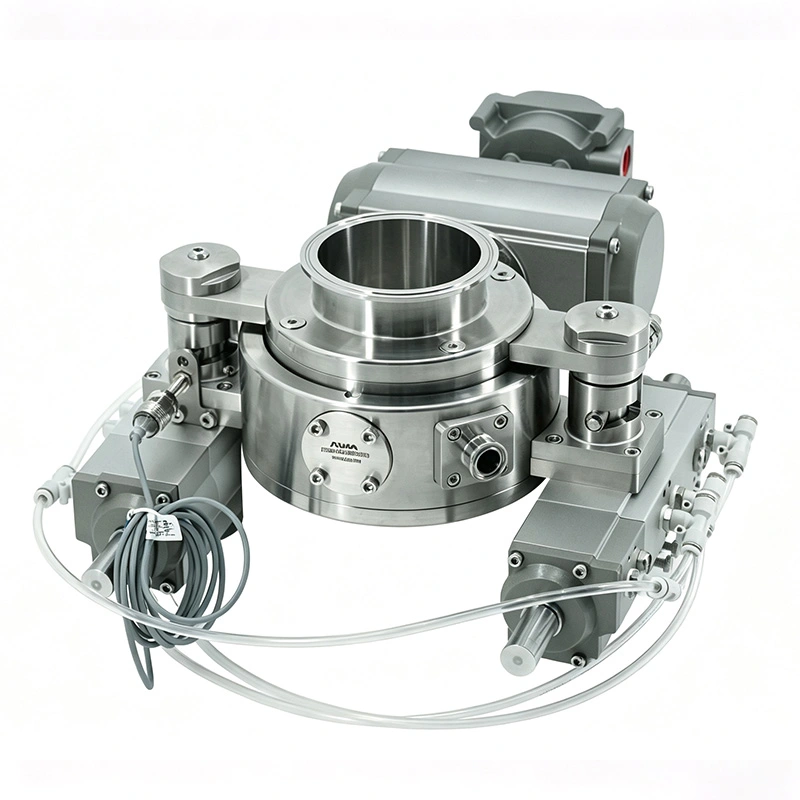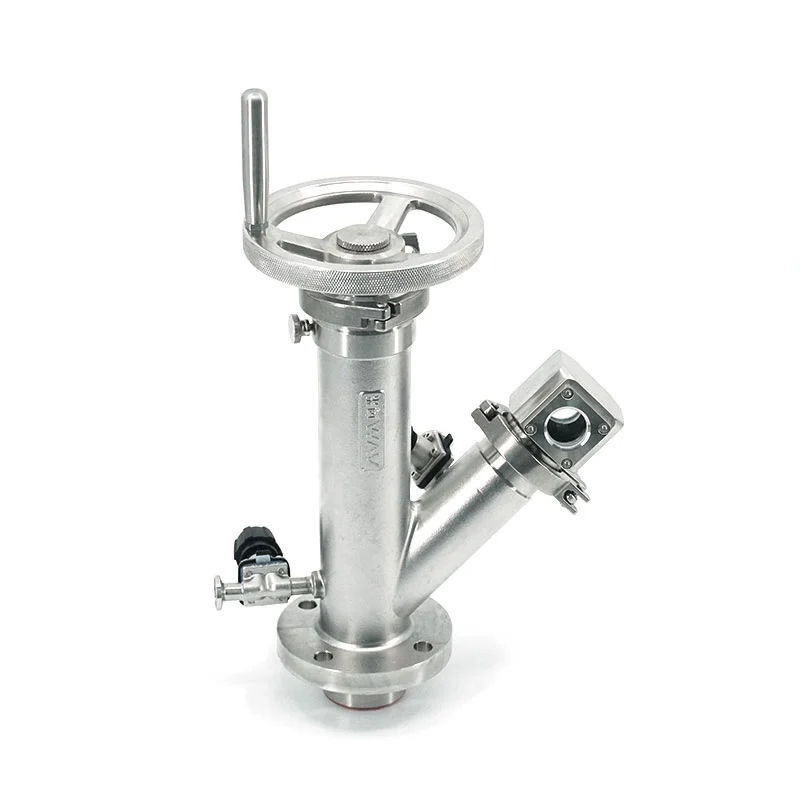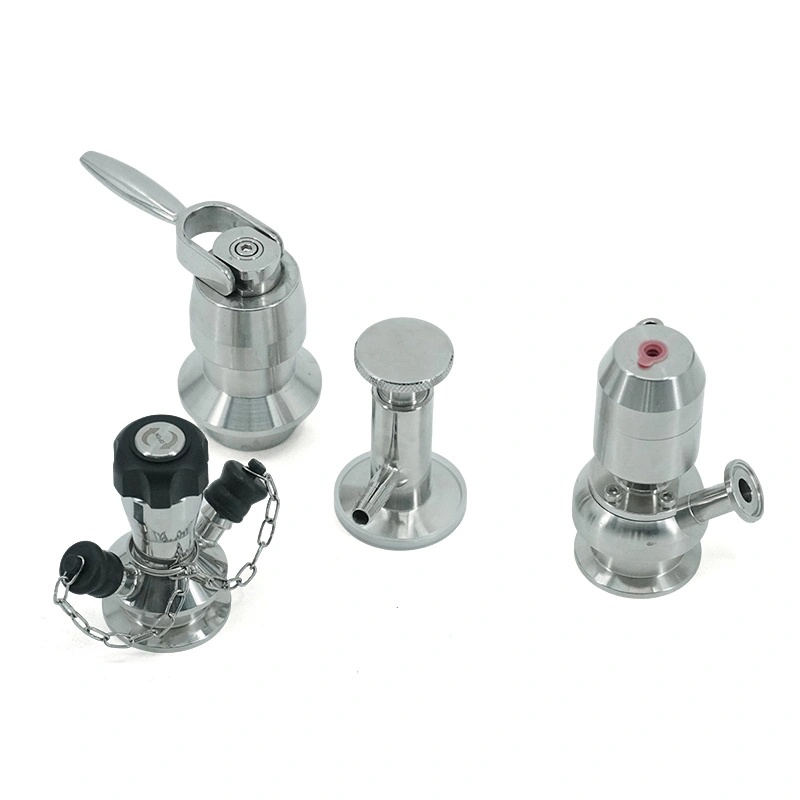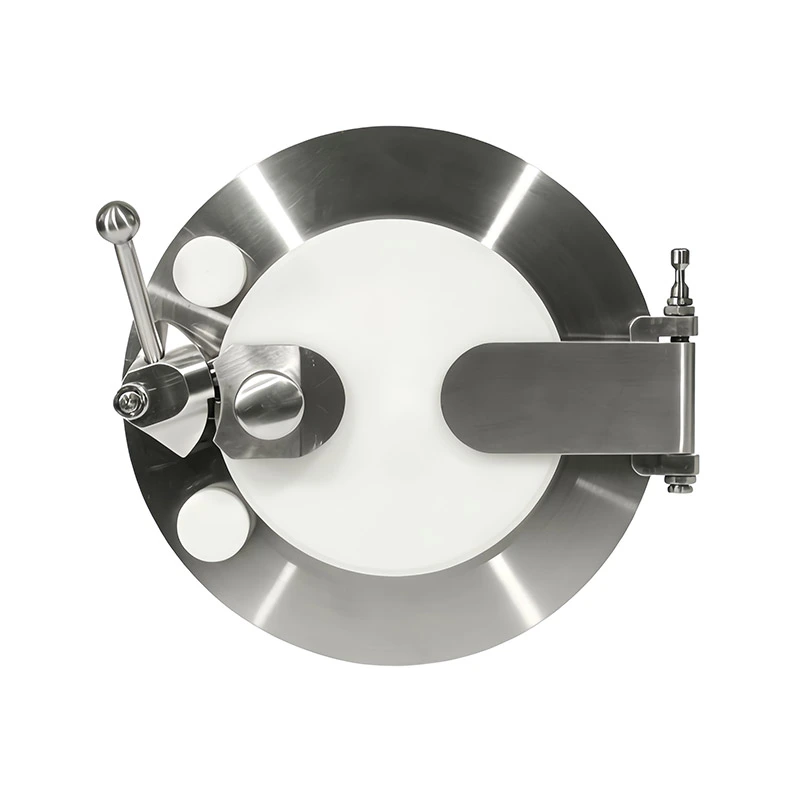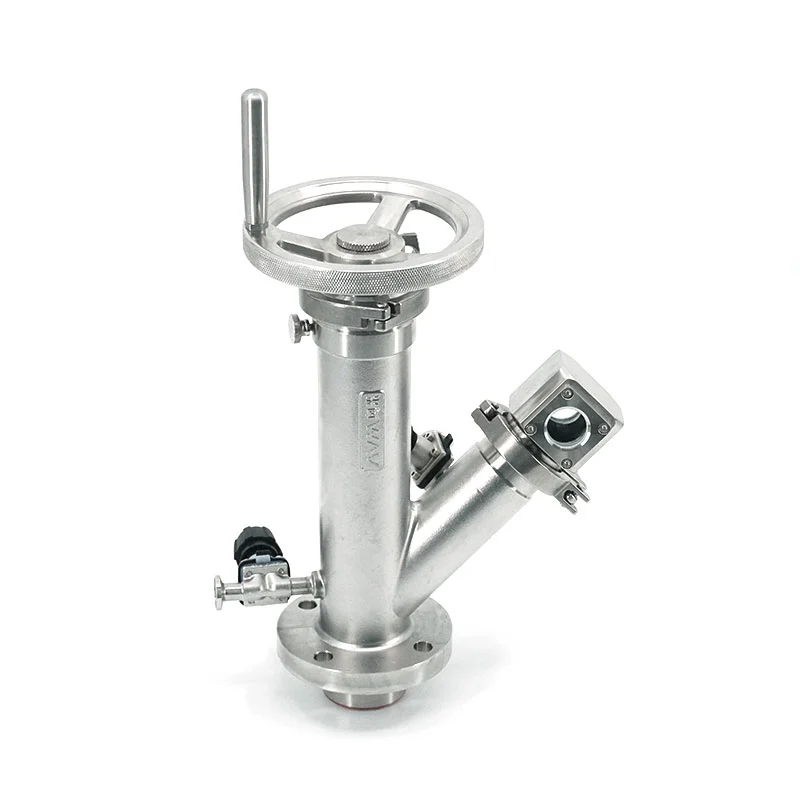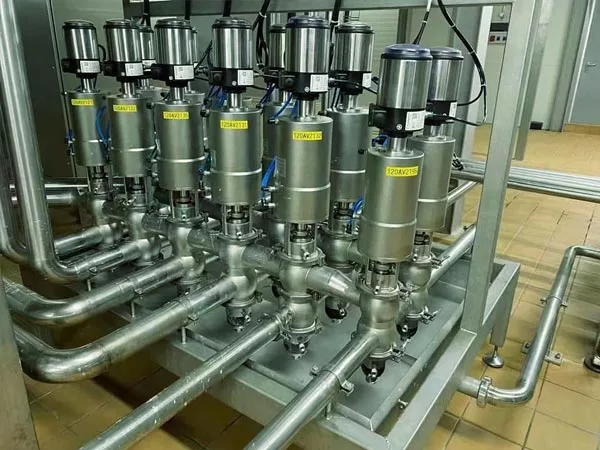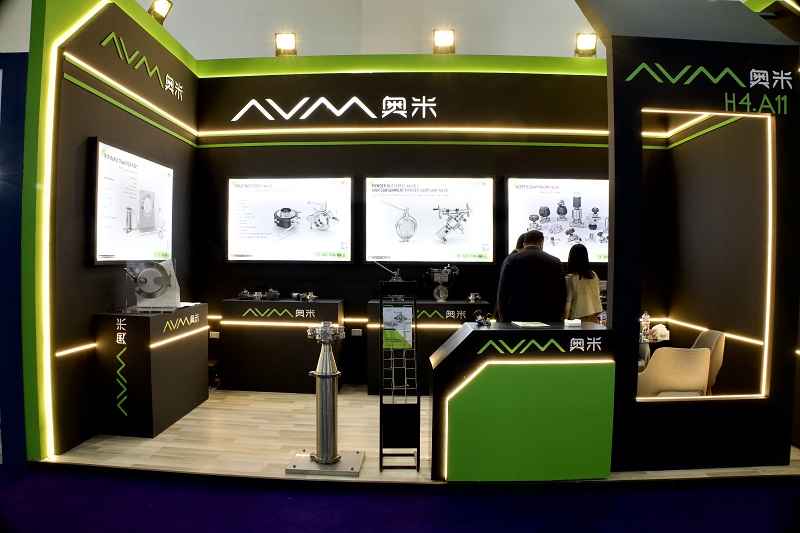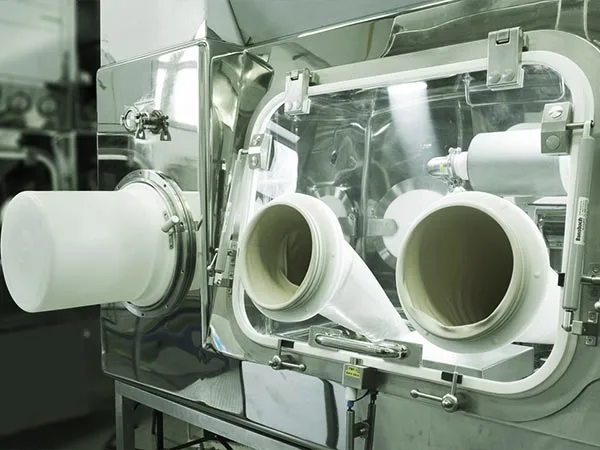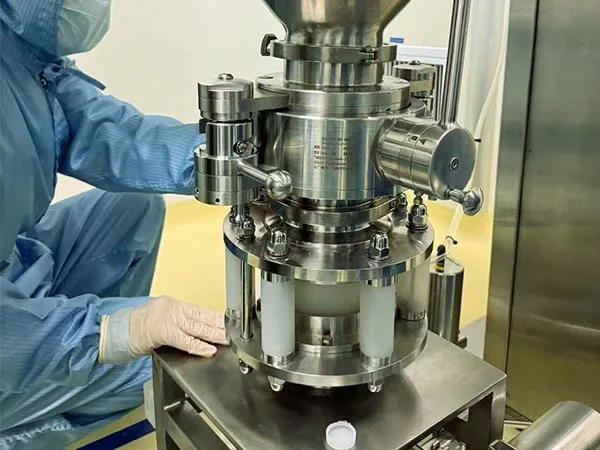
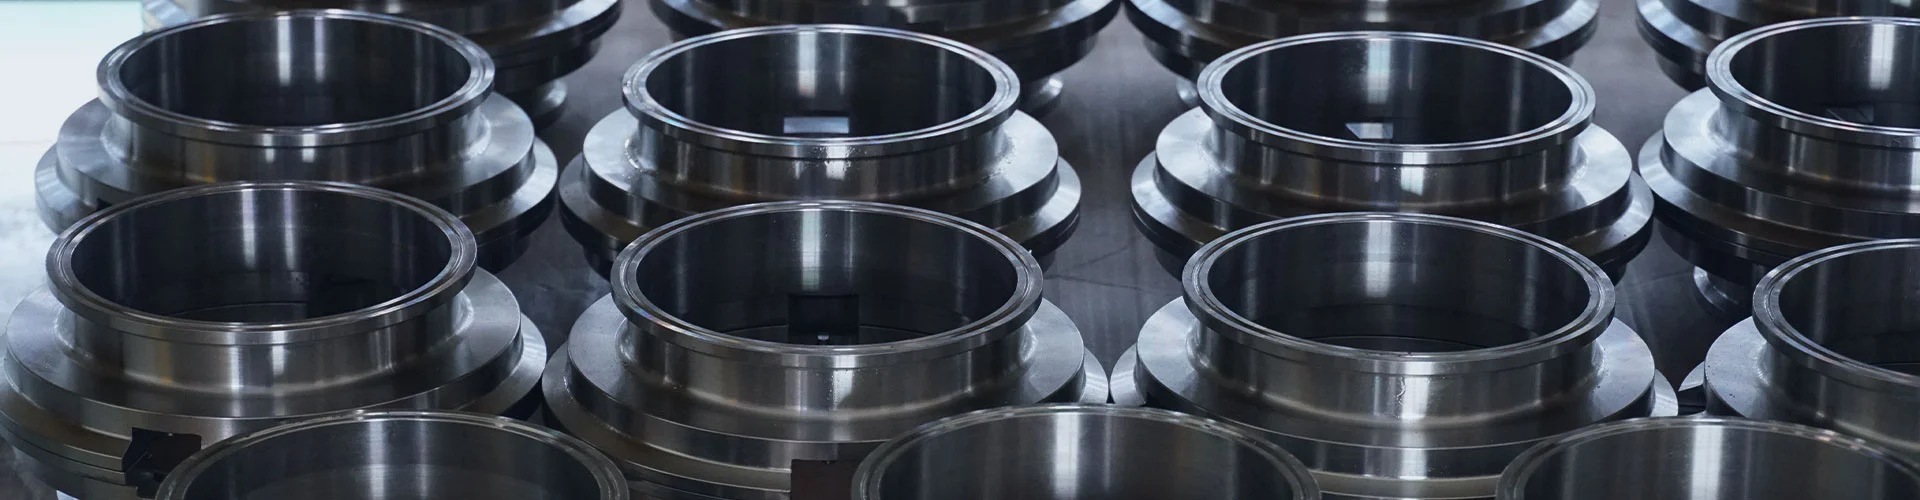
AVM provides containment solutions for pharmaceutical, food and beverage, fine chemical, and lithium battery production. Its sanitary valve range includes split butterfly valves (SBV), rapid transfer ports (RTP), contained sampling valves, and other configurations for controlled powder and liquid handling. The solutions focus on hygienic processing, containment performance, and reduced operator exposure.
AVM develops sanitary containment valve solutions for processes involving potent, toxic, or contamination-sensitive materials. The controlled transfer and isolation design helps reduce material release and operator exposure during production, making it suitable for applications where GMP and OEB requirements are important.
For production environments with strict hygiene requirements, AVM focuses on GMP-oriented sanitary construction to help reduce material retention and cross-contamination risks. The equipment can be configured for different powder and liquid handling processes according to media characteristics, cleaning procedures, connection requirements, and operating conditions.
In pharmaceutical manufacturing, the sanitary containment valve can be used for contained handling of potent or toxic materials. Food and beverage processors can apply it where hygienic material transfer and product protection are required. Fine chemical manufacturers can use containment solutions to control powder and liquid transfer, while lithium battery production can benefit from controlled material handling where cleanliness and contamination prevention are important.
A properly selected sanitary containment valve can help manufacturers reduce operator exposure, control material release, and maintain cleaner processing conditions. Its containment function also helps minimize the possibility of cross-contamination, which is particularly valuable when production lines handle multiple materials or high-potency products.
AVM Extraordinary Intelligence Control Co., Ltd. is located in Wenzhou, China, and integrates design, development, production, and sales. With experience serving pharmaceutical, food and beverage, fine chemical, and lithium battery industries, AVM provides containment valve solutions based on different process requirements. The company holds ISO 9001, CE, and FDA certifications, providing international buyers with recognized references for quality and product compliance.