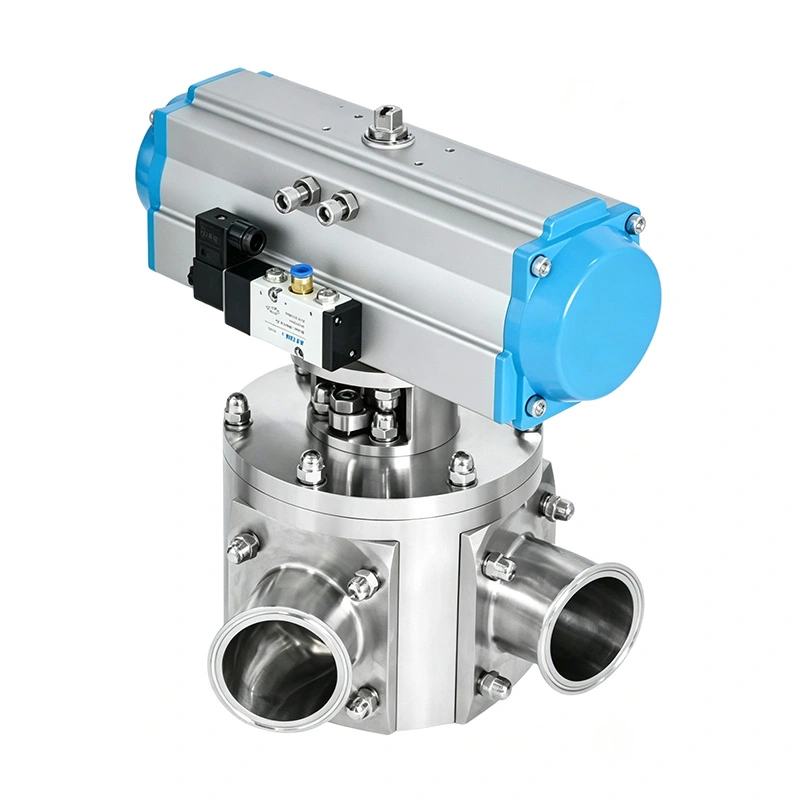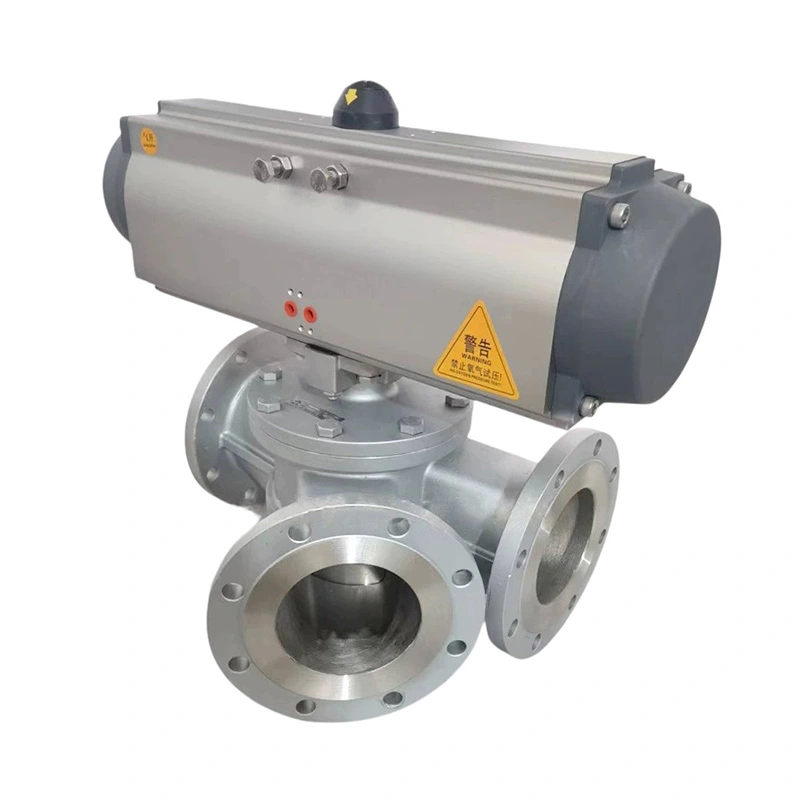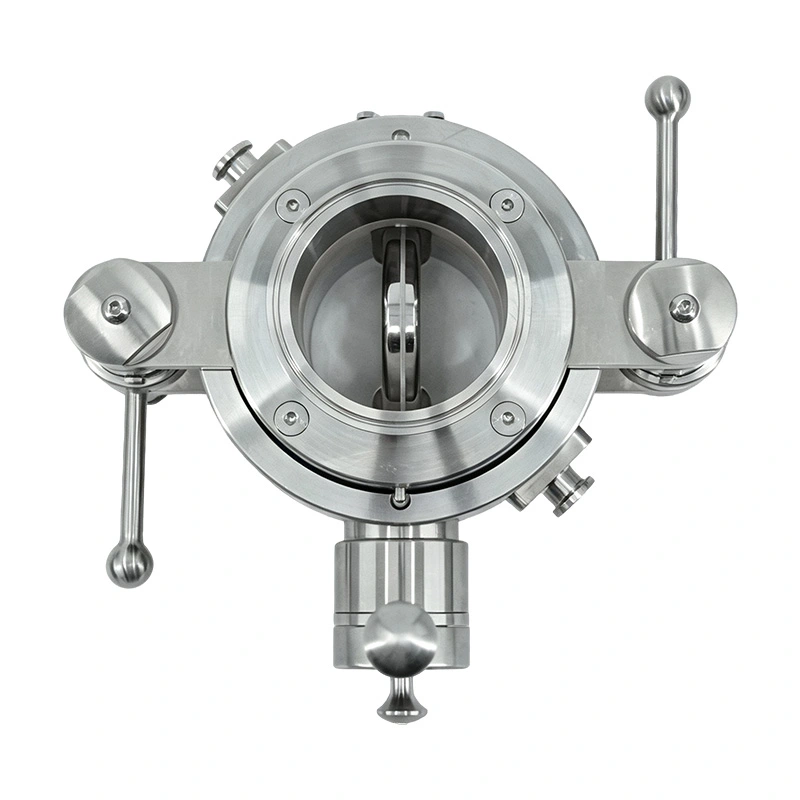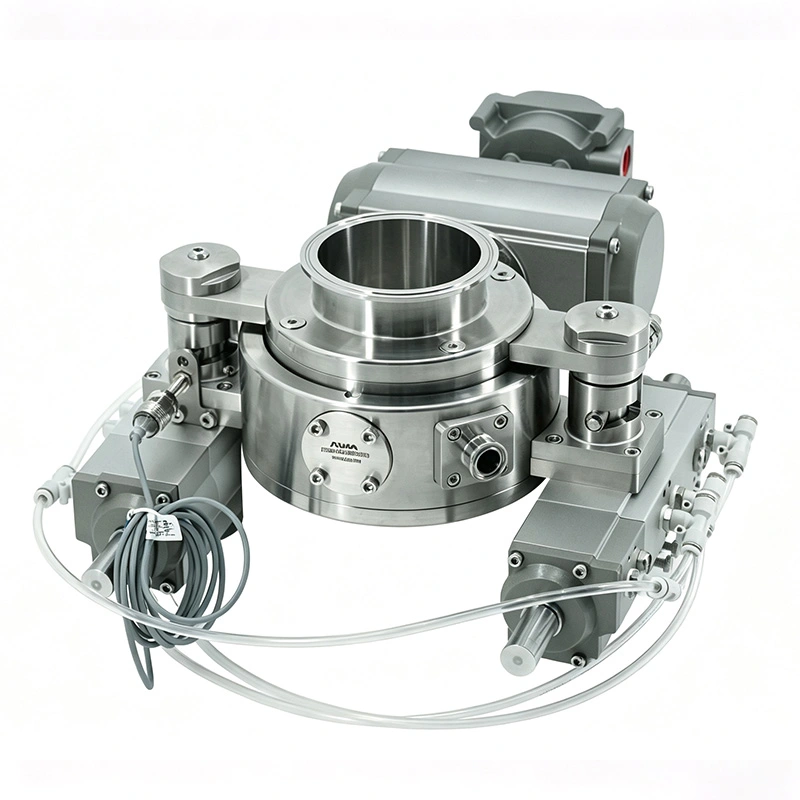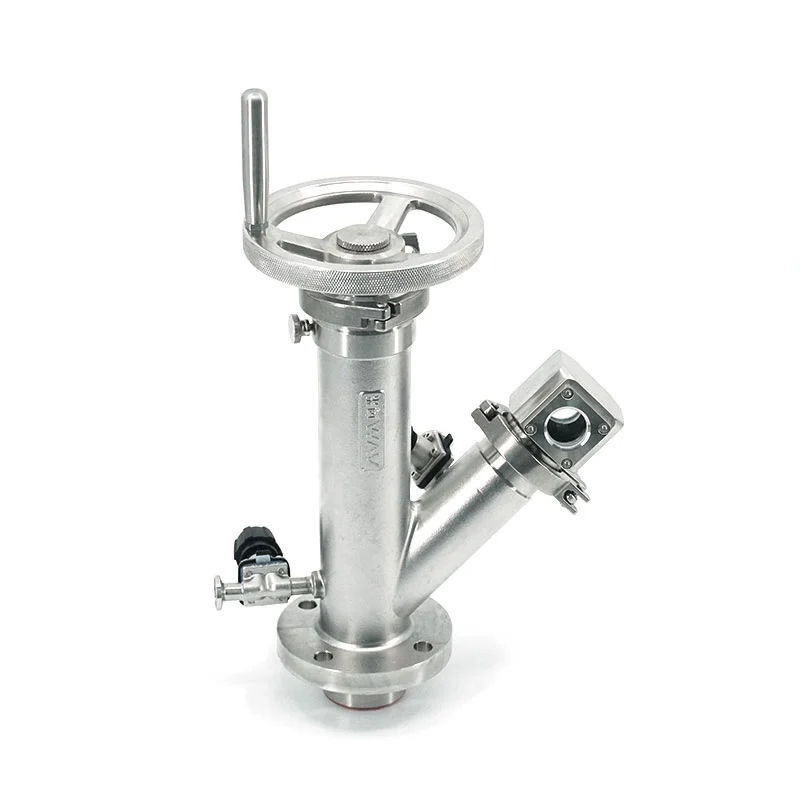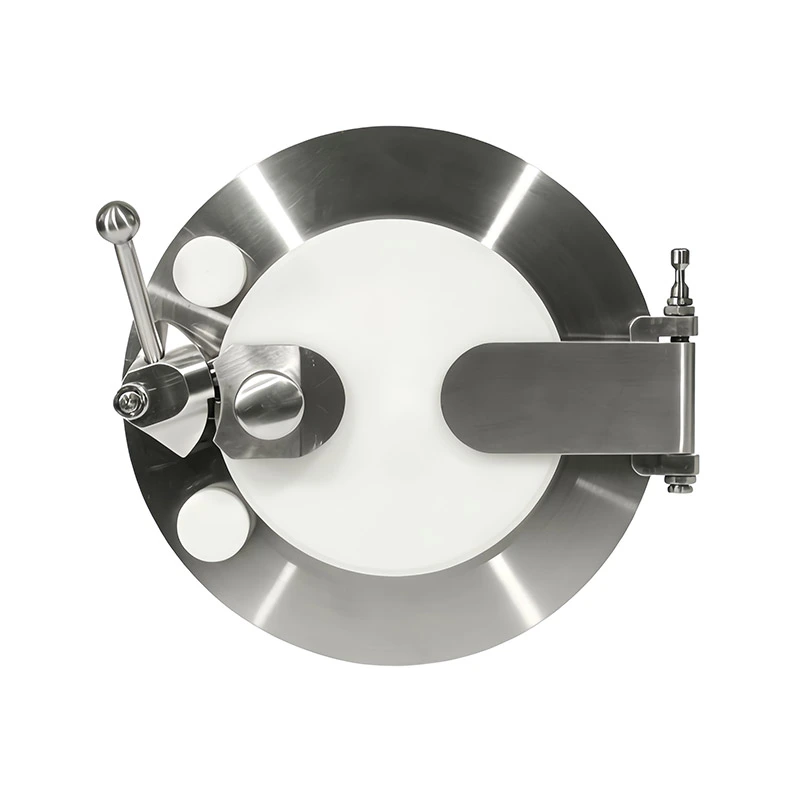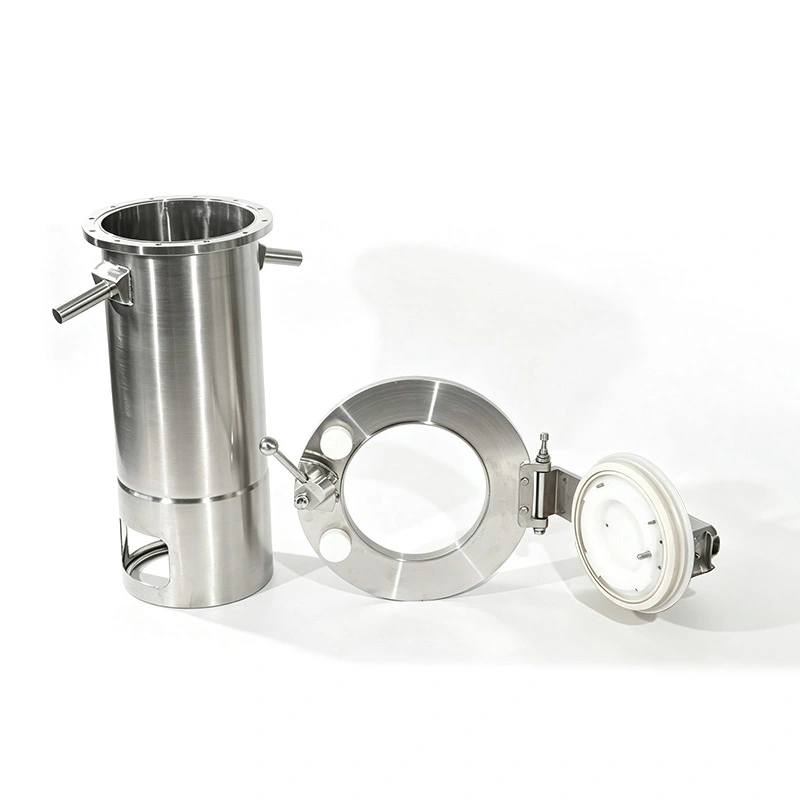
AVM provides sanitary flow routing solutions for pharmaceutical, food, chemical, biotechnology, and other high-cleanliness processing industries. The diverter valve is designed to control the direction of powders, granules, liquids, and other process materials between different pipelines or equipment units. It helps manufacturers create more flexible production layouts by managing multiple flow paths within a single valve system.
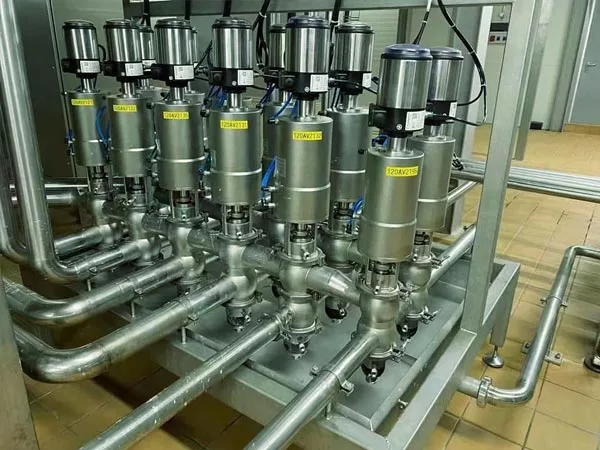
In many production systems, materials need to be transferred between different destinations according to process requirements. AVM's Sanitary Diverter Valve provides a practical solution for switching material flow paths, allowing one inlet to connect with different outlets or enabling controlled routing between multiple process sections. This helps reduce complex piping arrangements and improves system flexibility.
Modern production lines often include multiple stages such as feeding, mixing, drying, filling, and discharge. A suitable diverting solution allows operators to direct materials to the correct processing unit without manually changing pipeline connections. The Sanitary Diverter Valve can be integrated into automated systems to support repeatable material routing during different production steps.
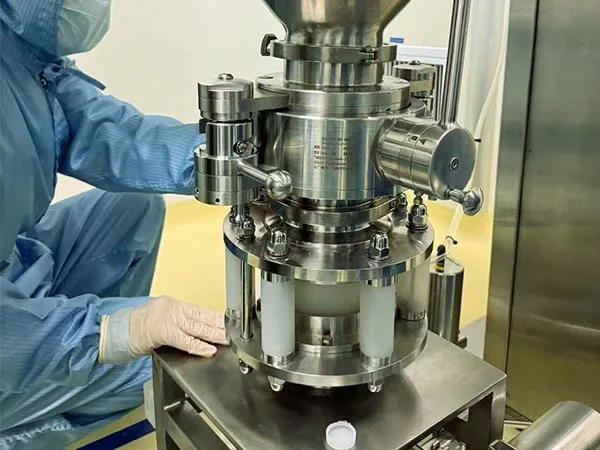
AVM designs valve solutions according to different equipment layouts and process requirements. The valves can be applied with mixers, dryers, filling machines, transfer systems, storage equipment, and other processing units. By matching the valve configuration with the complete production line, manufacturers can optimize space utilization and improve equipment coordination.
When different materials or production stages share the same process line, controlling the flow direction is important to avoid unwanted mixing between streams. AVM focuses on reliable switching performance to help maintain clear separation between different process routes. This makes the valve suitable for applications requiring controlled transfer of powders, granules, bulk solids, or liquid media.
AVM sanitary valve solutions are designed for various material handling processes, including powder transfer, dosing, sampling, dispensing, charging, discharging, mixing, drying, and filling. The Sanitary Diverter Valve can be selected according to material characteristics, flow direction requirements, cleaning procedures, and equipment connection conditions.
For pharmaceutical, food, and other high-cleanliness industries, valve construction needs to support hygienic operation. AVM develops sanitary designs with suitable materials and process compatibility to meet demanding production environments. The valve structure can help simplify equipment integration while supporting cleaner and more reliable material handling operations.
Different industries require different flow control strategies. Pharmaceutical manufacturers can use diverting solutions for controlled material movement between process units, while food, chemical, and biotechnology companies can apply suitable configurations according to their production requirements. AVM provides customized options based on system layout, operating conditions, and process objectives.
AVM Extraordinary Intelligent Control Co., Ltd. is located in Wenzhou, China, and specializes in sanitary valve design, development, manufacturing, and technical support. The company provides valve solutions for pharmaceutical, biotechnology, food, and chemical industries. AVM holds ISO 9001, CE, and FDA certifications, providing international buyers with additional references when evaluating sanitary process equipment suppliers.
For applications requiring a Sanitary Diverter Valve, AVM can provide suitable configurations based on flow direction, equipment arrangement, material characteristics, and production process requirements.