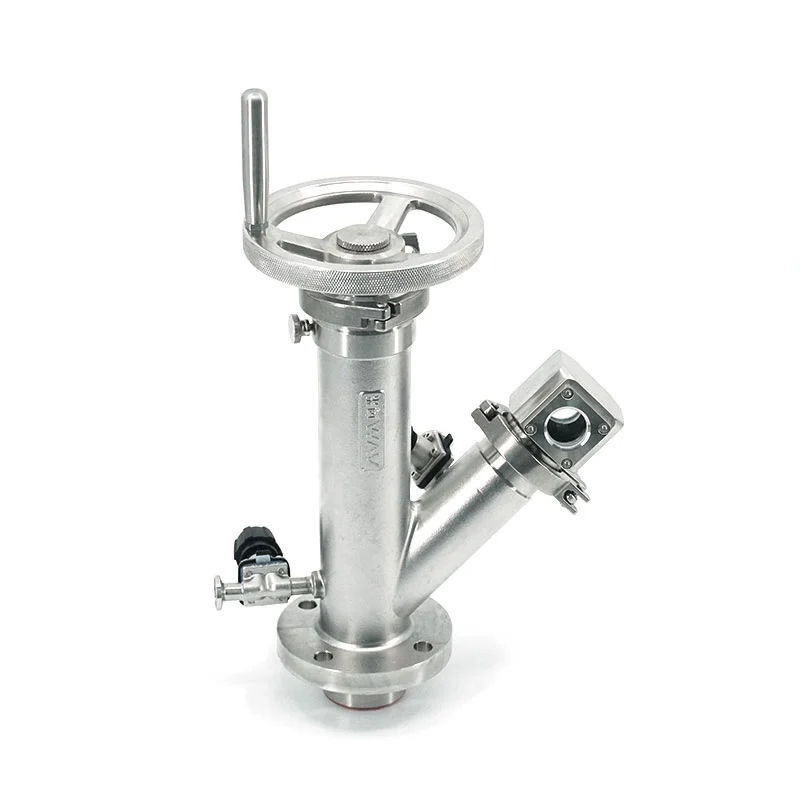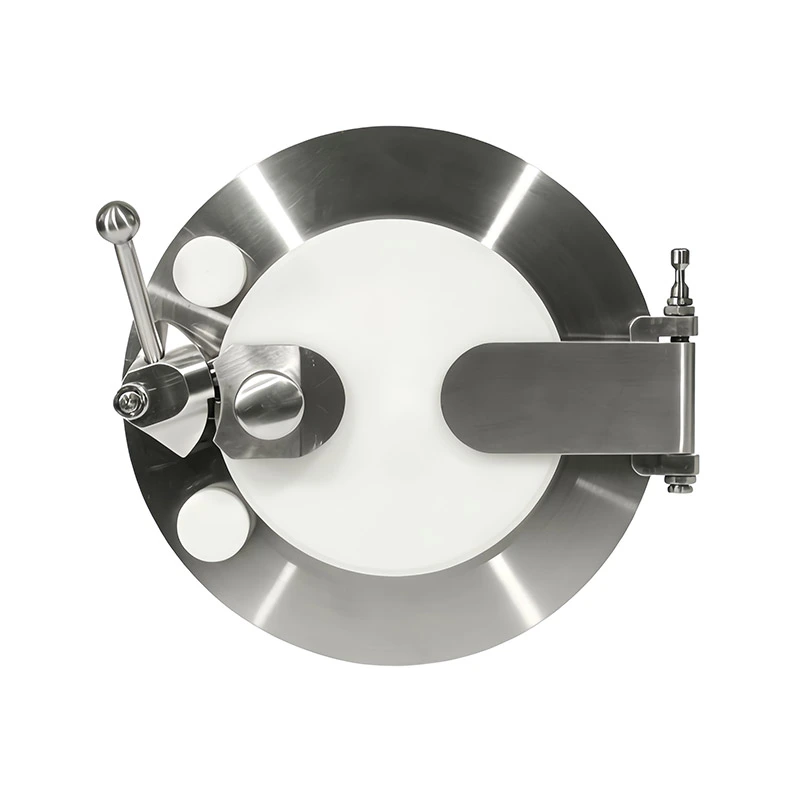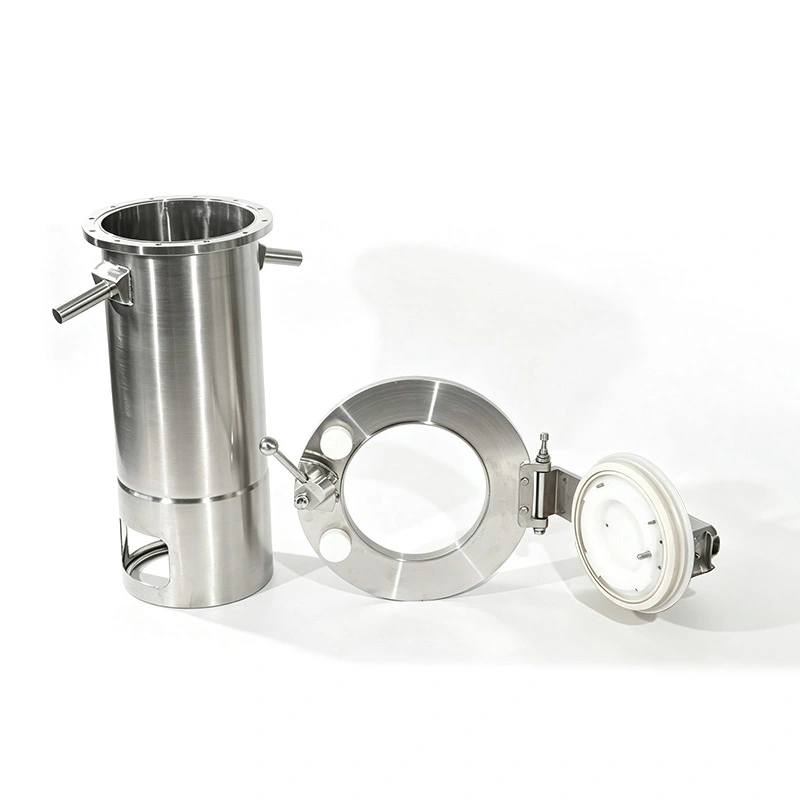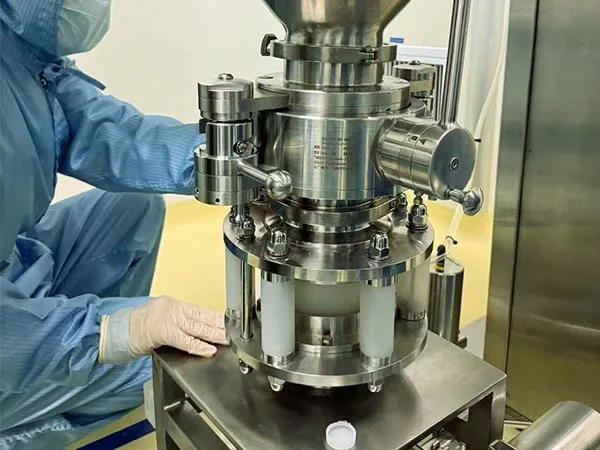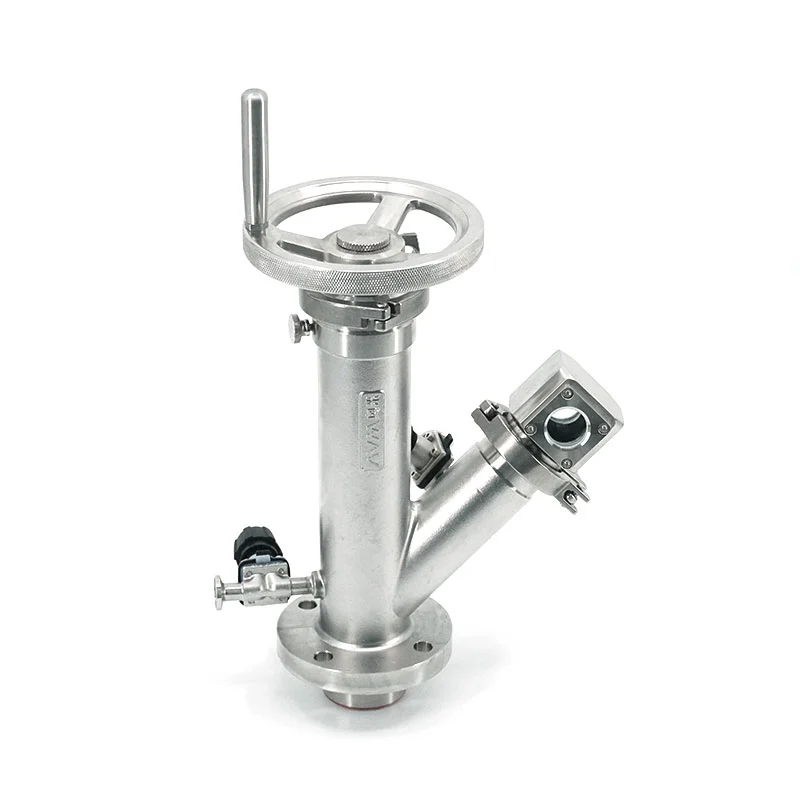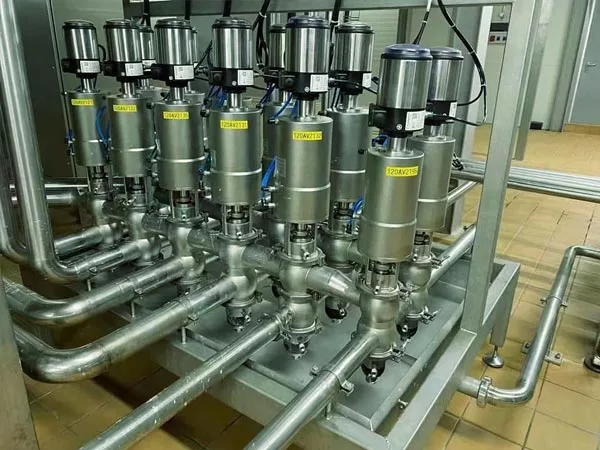
AVM provides hygienic and sterile valve solutions for pharmaceutical, food and beverage, fine chemical, lithium battery, and other high-cleanliness industries. The product portfolio covers valves for both powder and liquid process applications, including sanitary butterfly valves, sanitary ball valves, 3-way sanitary ball valves, powder handling valves, and containment valve solutions. Different valve structures allow manufacturers to select equipment according to media characteristics, pipeline layout, flow requirements, and process conditions.
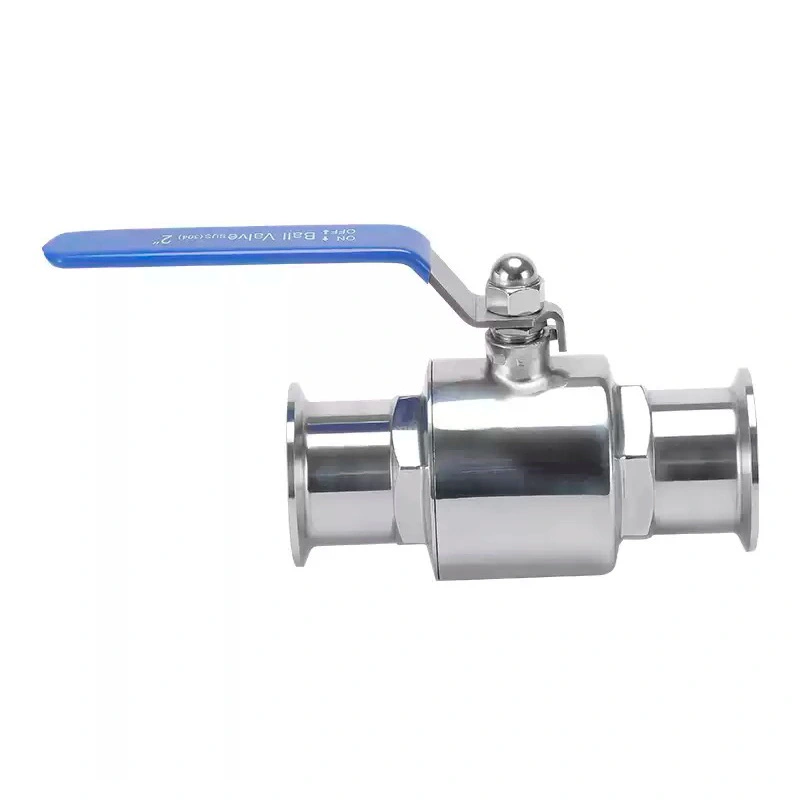
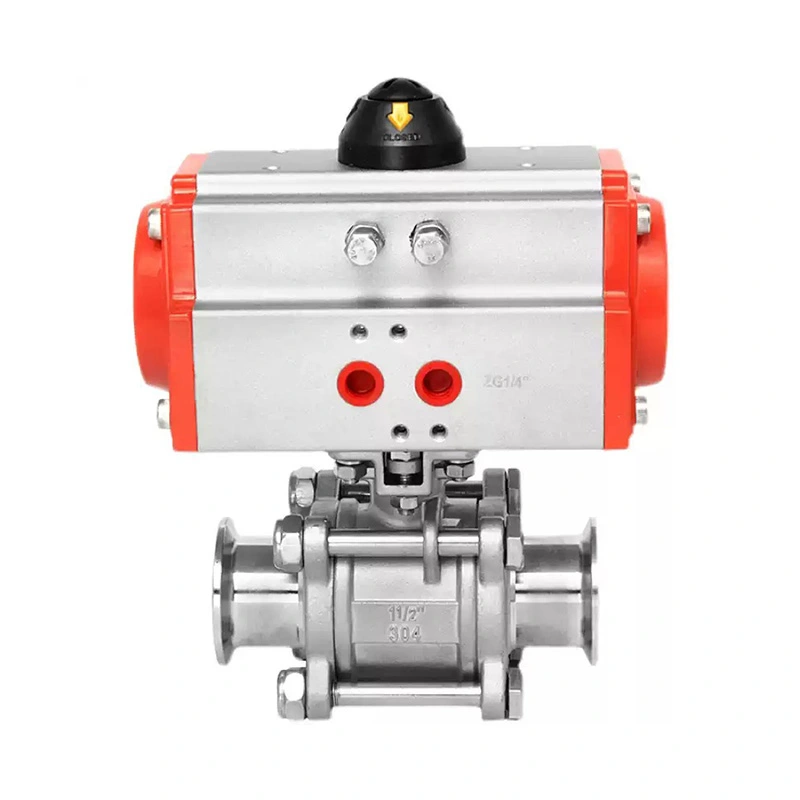
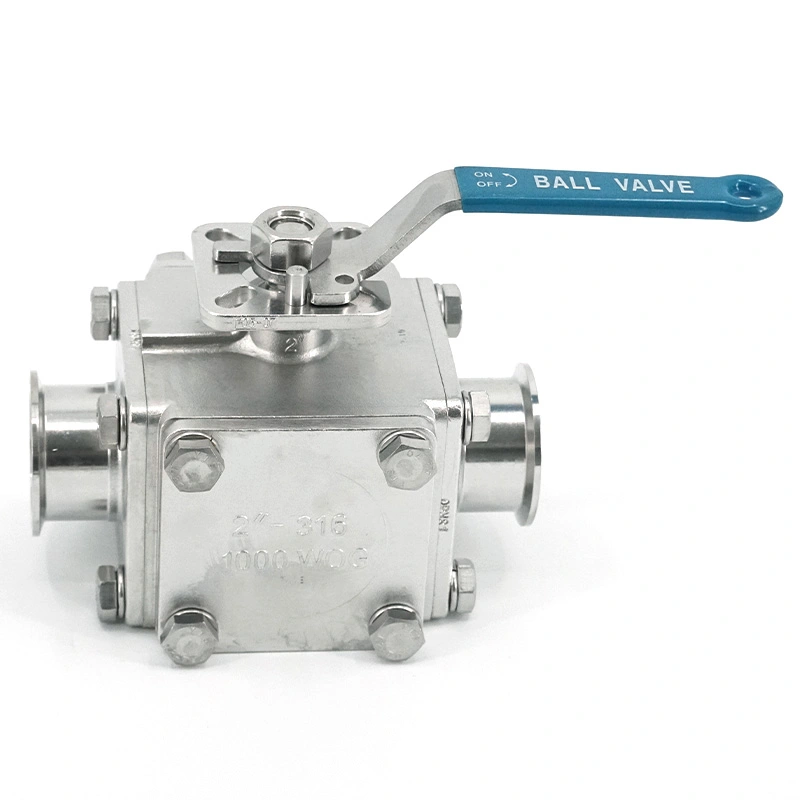
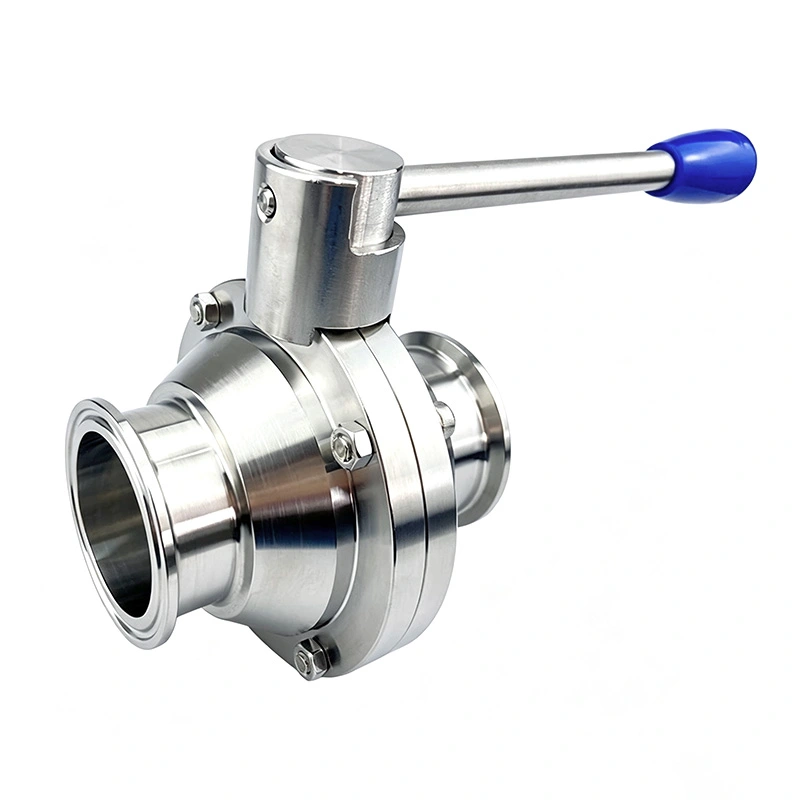
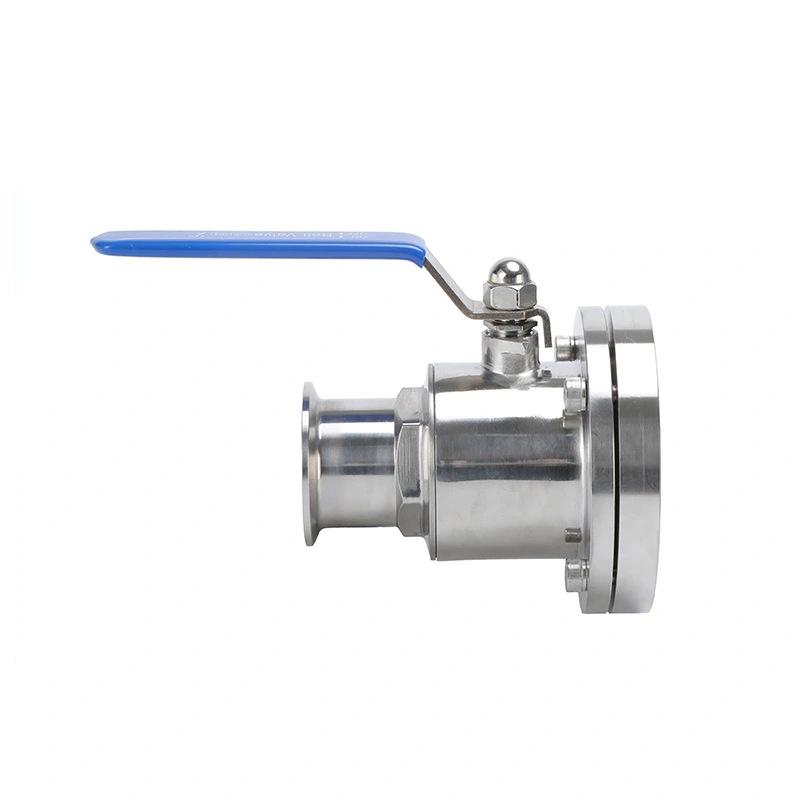
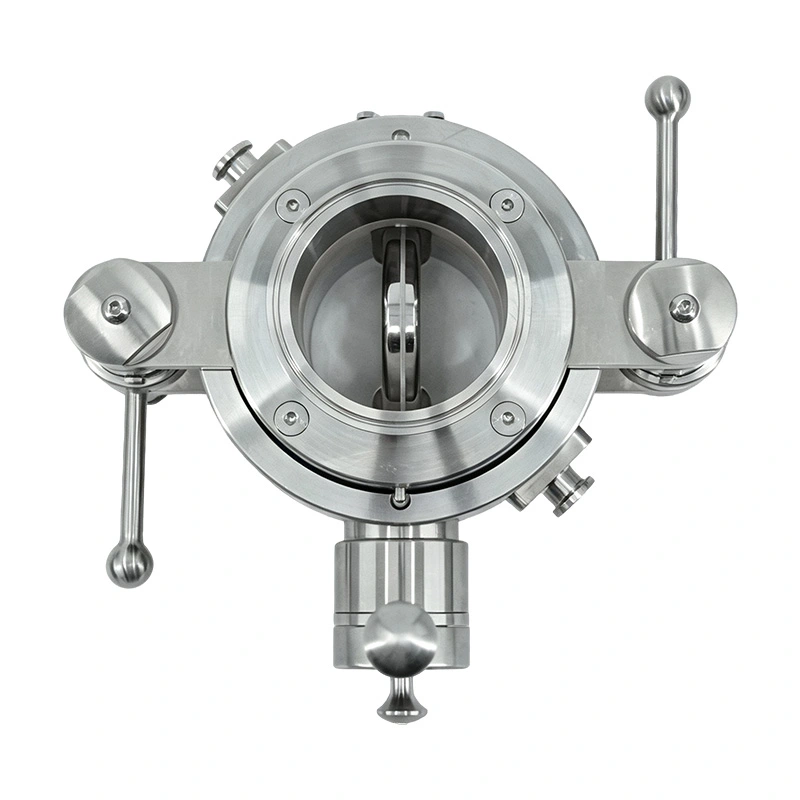
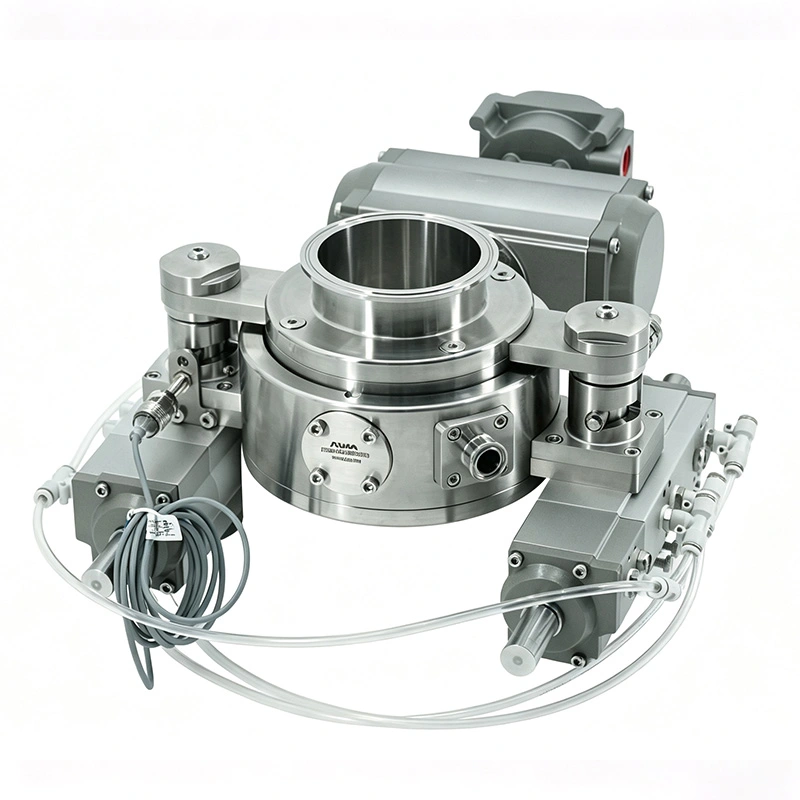
AVM's sanitary valve range includes 2-piece and 3-piece sanitary butterfly valves, V-type 2-piece sanitary ball valves, 3-piece sanitary ball valves, and 3-way sanitary ball valves with L-type and T-type ball configurations. The broader range also includes easy-clean powder butterfly valves, expansion butterfly valves, powder knife valves, segment valves, split butterfly valves, RTP systems, and contained sampling valves for specialized process requirements.
Sanitary processing systems may handle liquids, powders, cleaning media, ingredients, chemical materials, or pharmaceutical products with different flow characteristics. AVM offers multiple valve structures so buyers can select suitable equipment based on the material being processed, operating conditions, cleaning procedures, flow direction, and required isolation or transfer function.
Different process stages require different methods of controlling material movement. Butterfly valves provide compact solutions for pipeline isolation and general flow control, while ball valves offer alternative flow-path characteristics. For systems requiring pipeline diversion or combination, 3-way ball valves with L-type and T-type configurations provide additional flow-routing options.
Valve construction is an important consideration in high-cleanliness production because internal design can affect cleaning, maintenance, and process consistency. AVM develops its sanitary valve range for applications where hygienic operation and reliable process control are required, helping manufacturers build cleaner and more manageable piping systems.
AVM serves pharmaceutical manufacturers requiring hygienic and sterile process equipment, as well as food and beverage producers handling ingredients and process fluids. Fine chemical and lithium battery manufacturers can also select suitable valve configurations for their specific material transfer and pipeline requirements. The range is designed to support both standard sanitary processes and more specialized production environments.
AVM Extraordinary Intelligent Control Co., Ltd. is located in Wenzhou, China, and integrates product design, development, manufacturing, and technical support. As a specialized sanitary valve manufacturer, AVM provides different valve structures for powder and liquid handling applications. The company holds ISO 9001, CE, and FDA certifications, providing international buyers with recognized references when evaluating sanitary process equipment.