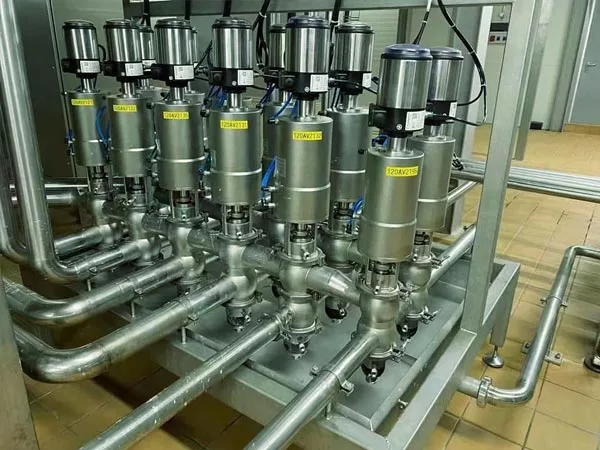
In biopharmaceutical, food, and fine chemical applications, the cleanability and sterilizability of fluid handling equipment directly impact product purity. Sanitary valves designed with full-bore, crevice-free configurations and CIP/SIP compatibility provide reliable control for high-purity fluid transfer.
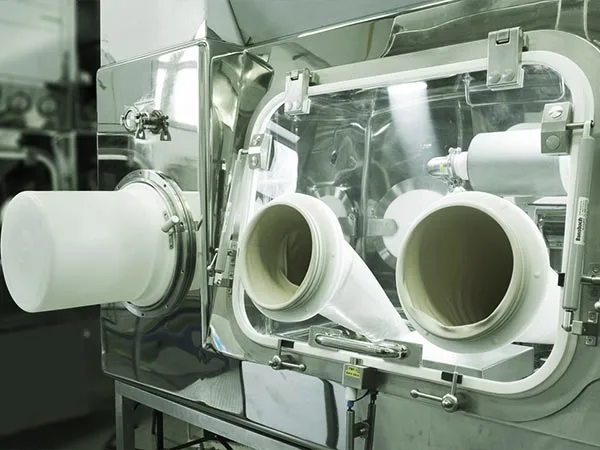
In sterile drug and biologic manufacturing, maintaining isolator or RABS integrity during material transfer is essential. RTP systems provide a standardized solution for this critical operation.
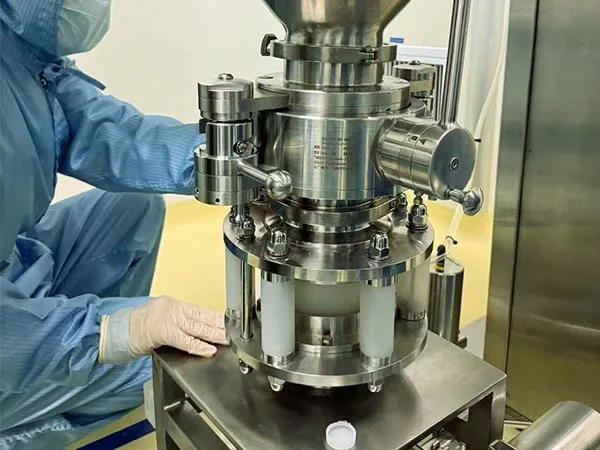
In the pharmaceutical and new energy industries, operator exposure and cross-contamination during powder transfer remain critical challenges. Split butterfly valve technology provides a reliable engineering solution for high-containment applications ranging from OEB 4 to OEB 5 performance levels.
We use cookies to offer you a better browsing experience, analyze site traffic and personalize content. By using this site, you agree to our use of cookies. Privacy Policy
 31 2026-07
 31 2026-07
 31 2026-07